ProductPRODUCT
Featured products
Contact Us
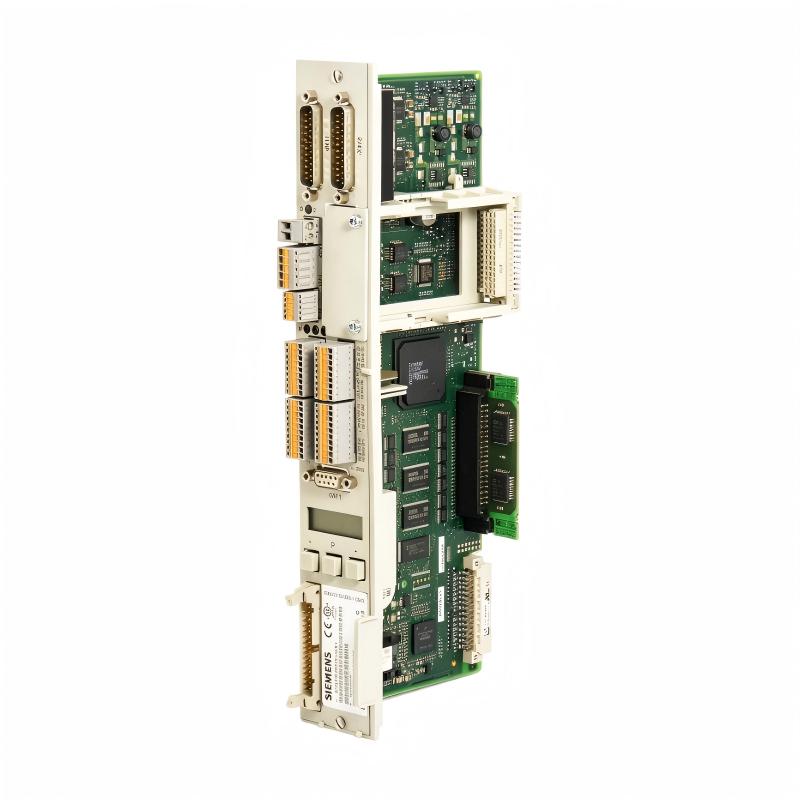
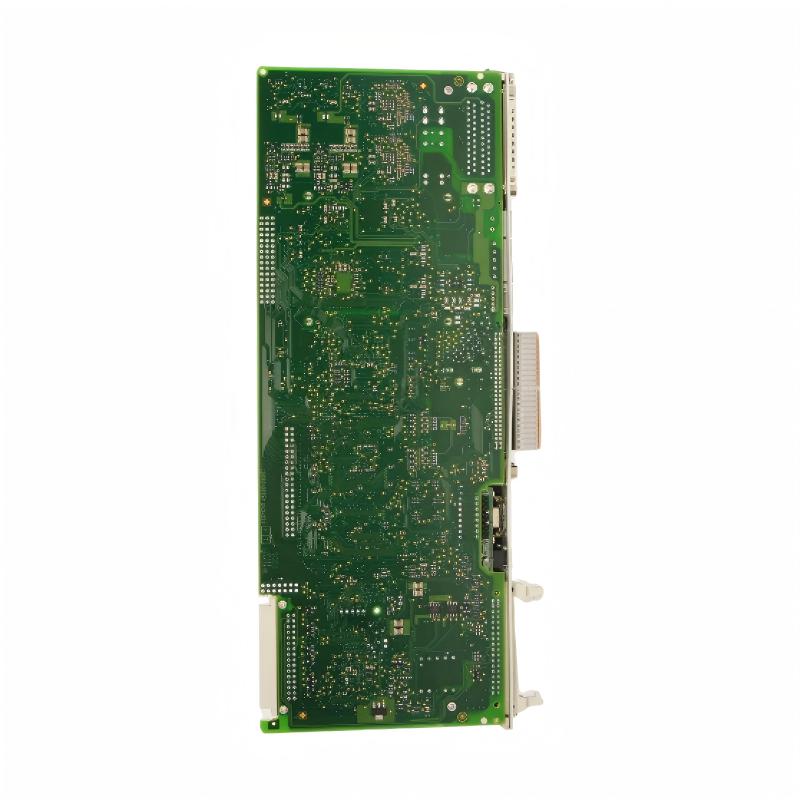
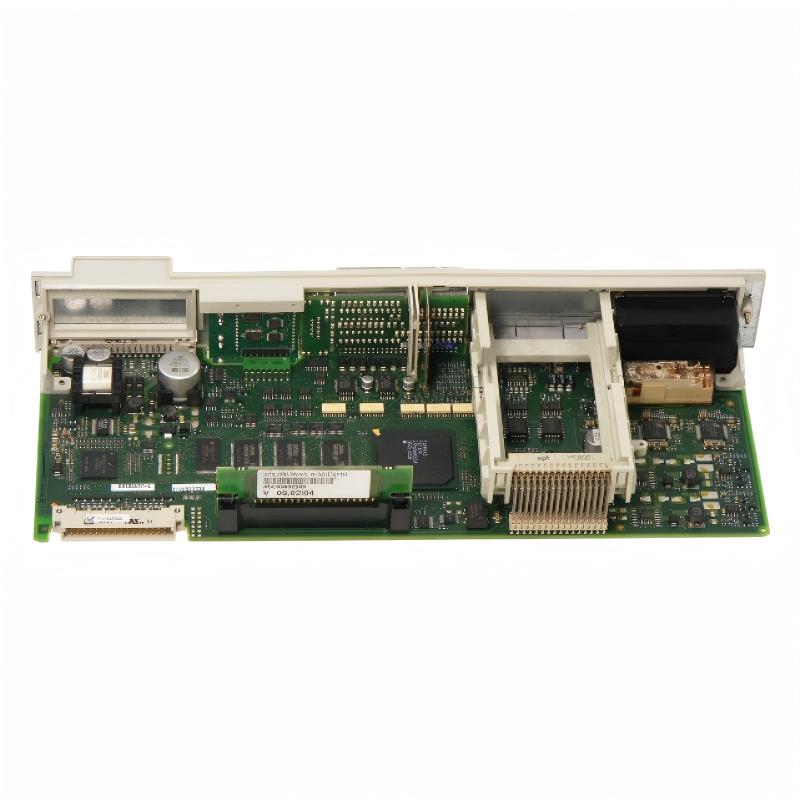
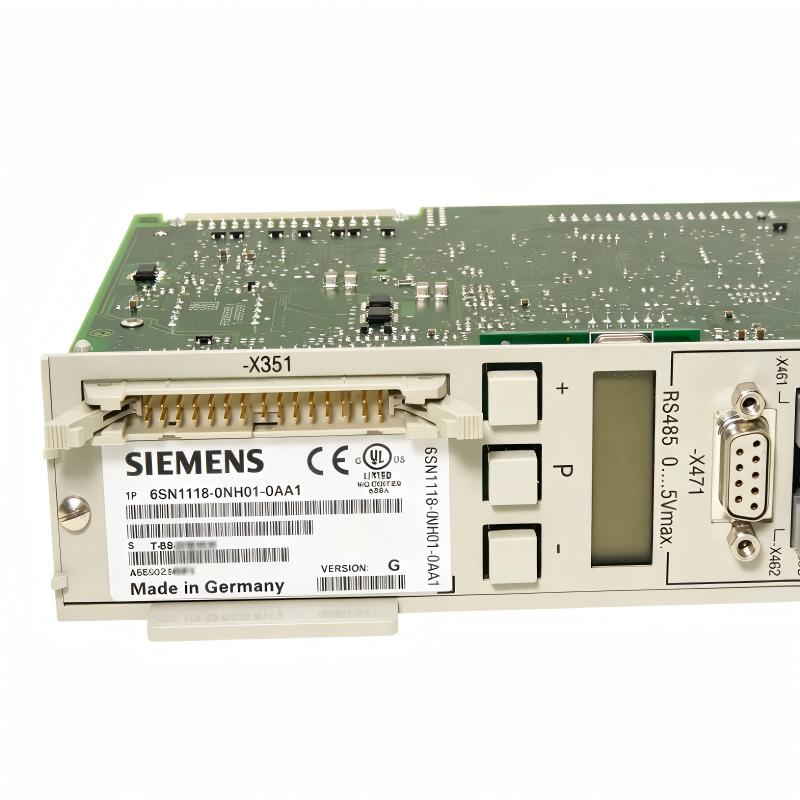
- Siemens
- 6SN1118-0NH01-0AA1
- Control Unit
- Germany
- 330 × 51 × 152 mm
- 0.57 kg
- Xiamen, China
- New & In Stock
- T/T, PayPal, Western Union
- 1 Year
- 1-3 Working Days
- DHL, UPS, TNT, FedEx and EMS.
- 24-Hour Service
- COO
- 8
Our advantage
Global Logistics
We have a 10-year logistics and express cooperation agreement, so our products can be shipped to any place in the world.
Brand new and original
Our products are imported in bulk from the place of origin. Because of the cooperative relationship, our products are all original and 100% new.
24-hour service
We provide 7*24 hours service to our customers. We will be there whenever you need us.
Price advantage
All our products are priced very favorably because we have our own warehouse and supply.
| Company Information | |||
| [email protected] | |||
| Mobile | +8615980777398 | ||
| +8615980777398 | |||
| 15980777398 |
Product Overview
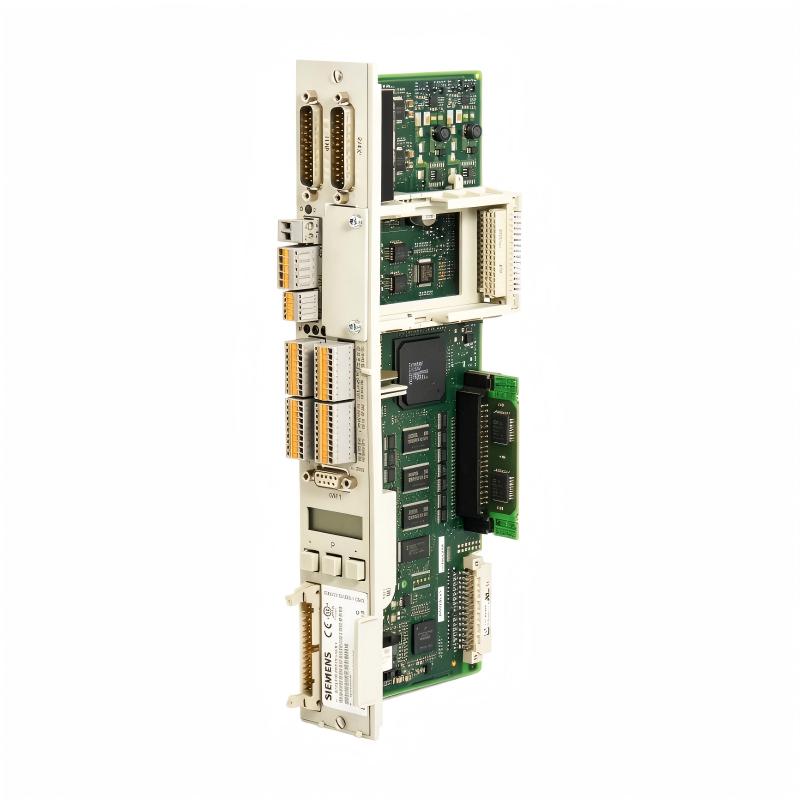
The Siemens 6SN1118-0NH01-0AA1 is a SIMODRIVE 611 Universal HR two-axis closed-loop control unit used in CNC machine tools and other drive systems requiring coordinated motor control. It supports incremental encoder signals, including SIN/COS 1 Vpp feedback, and compatible absolute-value encoders using EnDat. Its speed/torque setpoint functions allow it to process drive commands for supported feed-axis and spindle configurations. <Cite refs={[“turn700705search21″,”turn700705search24″,”turn700705search0”]}/>
In a CNC machining center, the control unit handles drive-control functions for the configured axes while the CNC controller determines the required motion. During a milling cycle, for example, the controller commands the cutting tool to follow a programmed path. The control unit processes the relevant setpoints and encoder feedback, and the associated power modules regulate the motors to produce the requested movement.
The NH01 configuration is part of the SIMODRIVE 611 Universal HR family. Its encoder interface is a key factor when matching the unit to an existing machine. A system using SIN/COS encoder feedback requires the appropriate signal connections and parameter settings; an installation using EnDat absolute encoders must likewise match the supported encoder configuration.
The two-axis designation refers to the unit’s control capability, although it can also be used in a single-axis application where the system configuration permits. This can be relevant when servicing machines with different axis arrangements within the same drive family. The actual application depends on the connected motors, power modules, feedback devices, and configured control functions.
When replacing an existing unit, check the complete order number and the machine’s feedback architecture. The control unit is one part of a modular drive system, so correct operation also depends on compatible hardware, suitable firmware, and properly restored drive parameters.
Technical Specifications
| Parameter | Specification |
|---|---|
| Manufacturer | Siemens |
| Model | 6SN1118-0NH01-0AA1 |
| Product Family | SIMODRIVE 611 Universal HR |
| Product Type | 2-Axis Closed-Loop Control Unit |
| Control Configuration | High Resolution (HR) |
| Number of Axes | 2 |
| Encoder Compatibility | Incremental encoders, SIN/COS 1 Vpp, and compatible absolute-value encoders with EnDat |
| Setpoint Interface | Speed/torque setpoint |
| Expansion Capability | Compatible optional modules |
| Drive Applications | Supported feed-drive and spindle-drive configurations |
| Installation Type | Plug-in control unit |
| Compatible System | SIMODRIVE 611 Universal |
| Dimensions | 330 × 51 × 152 mm |
| Weight | 0.57 kg |
Product Features
- Two-axis control capability: Supports two independent drive-control channels and can accommodate permitted single-axis configurations.
- High-resolution control architecture: Belongs to the SIMODRIVE 611 Universal HR range.
- Multiple feedback options: Supports compatible incremental, SIN/COS 1 Vpp, and EnDat encoder configurations.
- Speed/torque setpoint processing: Handles the configured drive commands for compatible motor applications.
- Optional module support: Allows supported terminal or communication functions to be added through compatible expansion hardware.
- CNC system integration: Connects the machine controller’s motion commands with the associated drive hardware.
- Parameter-based configuration: Requires correct axis assignments, encoder settings, and control parameters for the installed machine.
Working Principle
The 6SN1118-0NH01-0AA1 processes motion commands and encoder feedback within the SIMODRIVE 611 Universal drive architecture. The CNC controller issues the required movement commands, and the control unit works with the associated power modules to regulate motor operation.
A typical control arrangement is:
CNC Controller → 6SN1118-0NH01-0AA1 → SIMODRIVE Power Module → Motor → Machine Axis
Encoder Feedback → Control Unit → Closed-Loop Drive Regulation
During operation, the control unit evaluates the configured setpoint and feedback signals to regulate the motor’s response. The encoder reports movement information, allowing the drive system to compare actual motor movement with the requested motion and adjust its control output.
The feedback type affects how the machine must be configured. SIN/COS 1 Vpp encoders provide analog incremental signals, whereas EnDat absolute encoders use a different interface and data arrangement. These options are not interchangeable simply by changing a connector; the control hardware, wiring, and parameters must support the selected encoder.
For a two-axis milling application, the control unit processes the feedback and setpoints associated with the configured axes. If one axis begins to deviate from its expected movement, the diagnostic process should include encoder signals, drive parameters, power-module status, and the mechanical transmission. A feedback problem can resemble a motor or mechanical fault, so the measurement chain should be checked before replacing hardware.
The control unit does not independently perform every function in the machine’s automation system. CNC interpolation, machine sequencing, power conversion, and safety functions depend on their respective control and drive components.
Role in the SIMODRIVE 611 Universal Drive Architecture
The 6SN1118-0NH01-0AA1 sits in the drive-control layer of a modular CNC system. It processes the configured motion commands and feedback signals, while the CNC controller, power modules, motors, and optional interfaces provide the surrounding functions.
CNC Controller → Universal HR Control Unit → Power Module → Motor → Machine Axis
| System Element | Function |
|---|---|
| CNC Controller | Generates motion commands and coordinates machining operations |
| 6SN1118-0NH01-0AA1 | Processes two-axis closed-loop control and feedback information |
| SIMODRIVE 611 Power Module | Supplies controlled electrical power to compatible motors |
| Feed Motor or Spindle Motor | Produces the required mechanical movement |
| SIN/COS 1 Vpp Encoder | Supplies incremental movement feedback |
| EnDat Absolute Encoder | Provides supported absolute-position information |
| Optional Interface Module | Adds compatible terminal or communication functions |
| Drive Parameters | Define axis assignments, feedback scaling, and control behavior |
| CNC Electrical Cabinet | Houses the control unit and associated drive equipment |
Industrial Applications
| Application | Practical Use |
|---|---|
| CNC Milling Machines | Controlling compatible feed axes during programmed machining |
| CNC Turning Machines | Supporting configured feed and spindle-drive arrangements |
| CNC Machining Centers | Coordinating movement across two controlled axes |
| Precision Positioning Equipment | Regulating movement using compatible encoder feedback |
| Metalworking Production Lines | Integrating closed-loop drive control into CNC machinery |
| Machine Tool Retrofit Projects | Replacing a unit when the encoder and drive configuration match |
| Automated Manufacturing Machinery | Coordinating motor movement with machine-control commands |
| Modular SIMODRIVE Installations | Providing axis control within a larger drive architecture |
Installation and Maintenance
- Verify the complete order number: Confirm 6SN1118-0NH01-0AA1 and distinguish it from NH-series variants with different hardware or firmware configurations.
- Check the axis arrangement: Confirm whether the application uses one or two axes and verify compatibility with the installed power modules.
- Identify the encoder type: Determine whether the feedback devices use incremental signals, SIN/COS 1 Vpp signals, or a compatible EnDat absolute interface.
- Verify the feedback connections: Check connector assignments, cable condition, and signal requirements against the installed encoder configuration.
- Review optional modules: Identify any terminal or communication modules installed in the control unit and confirm that the configuration matches the machine design.
- Isolate the drive system: Follow the approved shutdown, electrical isolation, and DC-link discharge procedures before accessing the equipment.
- Inspect connectors and cables: Look for loose contacts, damaged insulation, contamination, and wiring faults that could affect feedback or control signals.
- Back up existing parameters: Preserve axis assignments, encoder settings, and relevant drive configuration data before replacement.
- Verify software compatibility: Confirm that the installed firmware and commissioning software support the intended control-unit configuration.
- Check feedback direction and scaling: Ensure that encoder signals correspond to the expected motor direction and configured engineering units.
- Test axis operation: Commission the configured axis or axes under controlled conditions and verify movement, feedback response, and fault indications.
- Record the final configuration: Document the order number, encoder types, optional modules, parameter settings, and commissioning results for future troubleshooting.
Compatible System Components
| Component | Function |
|---|---|
| Siemens 6SN1118-0NH01-0AA1 | Provides two-axis SIMODRIVE 611 Universal HR control |
| SIMODRIVE 611 Power Modules | Supply controlled electrical power to compatible motors |
| CNC Controller | Generates motion commands and coordinates machine operation |
| Compatible Feed Motors | Produce movement for configured feed axes |
| Compatible Spindle Motors | Support spindle operation in suitable drive configurations |
| SIN/COS 1 Vpp Encoders | Supply compatible incremental feedback signals |
| EnDat Absolute Encoders | Provide supported absolute-position feedback |
| SIMODRIVE 611 TERMINALS Option | Adds compatible terminal functions |
| SIMODRIVE 611 PROFIBUS-DP Option | Provides supported PROFIBUS-DP communication when configured with the appropriate module |
| Drive Parameter Configuration | Defines axis behavior, feedback scaling, and control settings |
Recommended Related Models
| Model | Product Type | Typical Application |
|---|---|---|
| Siemens 6SN1118-0NH01-0AA0 | SIMODRIVE 611 Universal HR 2-Axis Control Unit | Comparing the related two-axis control-unit variant |
| Siemens 6SN1118-1NH01-0AA1 | SIMODRIVE 611 Universal HR 2-Axis Positioning Control Unit | Applications requiring the corresponding positioning configuration |
| Siemens 6SN1118-0NK01-0AA1 | SIMODRIVE 611 Universal HR 2-Axis Resolver Control Unit | Drive systems using compatible resolver feedback |
| Siemens 6SN1118-1NK01-0AA1 | SIMODRIVE 611 Universal HR 2-Axis Positioning Control Unit for Resolvers | Two-axis positioning applications using resolver feedback |
| Siemens 6SN1118-0NJ01-0AA1 | SIMODRIVE 611 Universal HR 1-Axis Resolver Control Unit | Single-axis applications using compatible resolver feedback |
| Siemens 6SN1114-0NA00-0AA0 | SIMODRIVE 611 TERMINALS Option Module | Adding supported terminal functions to a compatible control-unit configuration |
Key Advantages
- Supports two-axis closed-loop control within the SIMODRIVE 611 Universal HR system.
- Accommodates compatible SIN/COS 1 Vpp and EnDat feedback configurations.
- Processes speed/torque setpoints for supported drive applications.
- Allows compatible terminal or communication expansion.
- Integrates with modular CNC drive hardware and machine-control systems.
Technical FAQs
How does the 6SN1118-0NH01-0AA1 differ from the 6SN1118-1NH01-0AA1?
The 0NH01 variant is the n-set control version, while the 1NH01 variant is identified as a positioning control unit. The required control function should match the machine’s drive architecture and motion-control requirements.
Can this unit operate with a single drive axis?
Yes. Although it is a two-axis control unit, the SIMODRIVE documentation permits one-axis operation for two-axis control boards. The power-module arrangement and parameter configuration must still match the intended application.
What should be checked when switching between SIN/COS and EnDat feedback?
Verify the encoder interface, signal wiring, supported feedback configuration, and drive parameters. The two feedback types use different signal arrangements, so the change must be supported by the installed hardware and software rather than treated as a wiring-only substitution.
Why might a connected axis fail to follow its command after the control unit is replaced?
Check the stored drive parameters, axis assignment, encoder configuration, feedback direction, and power-module status. Incorrect feedback scaling or an incompatible encoder configuration can prevent the drive from responding as expected even when the replacement unit is installed correctly.