ProductPRODUCT
Featured products
Contact Us
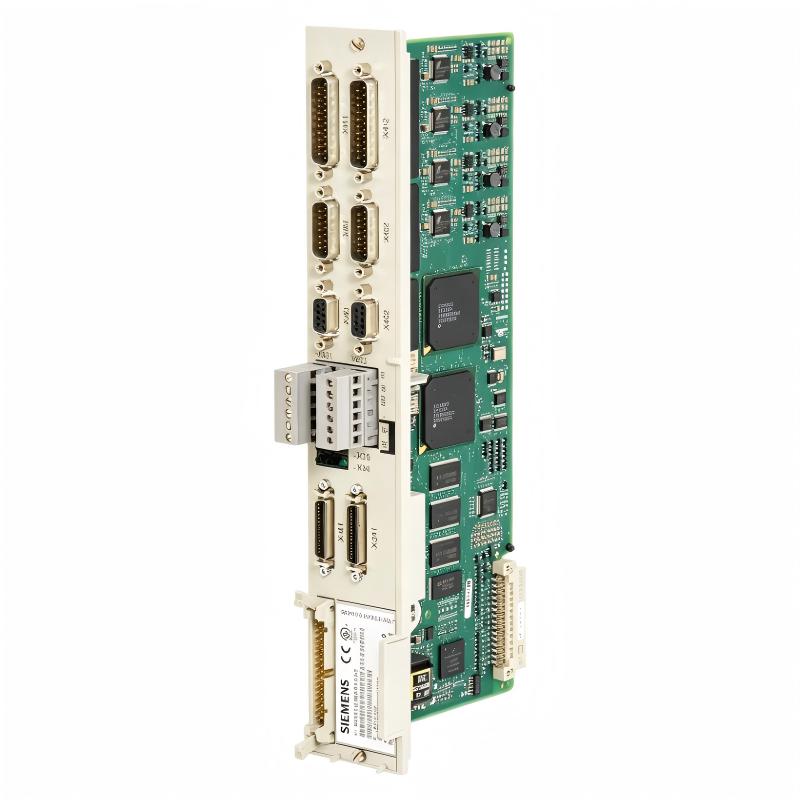
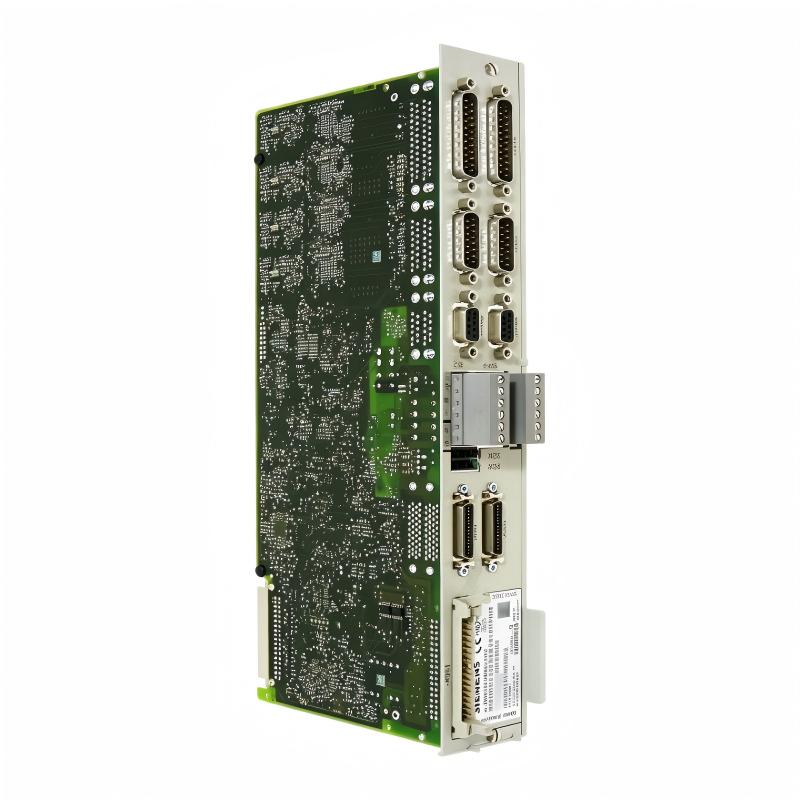
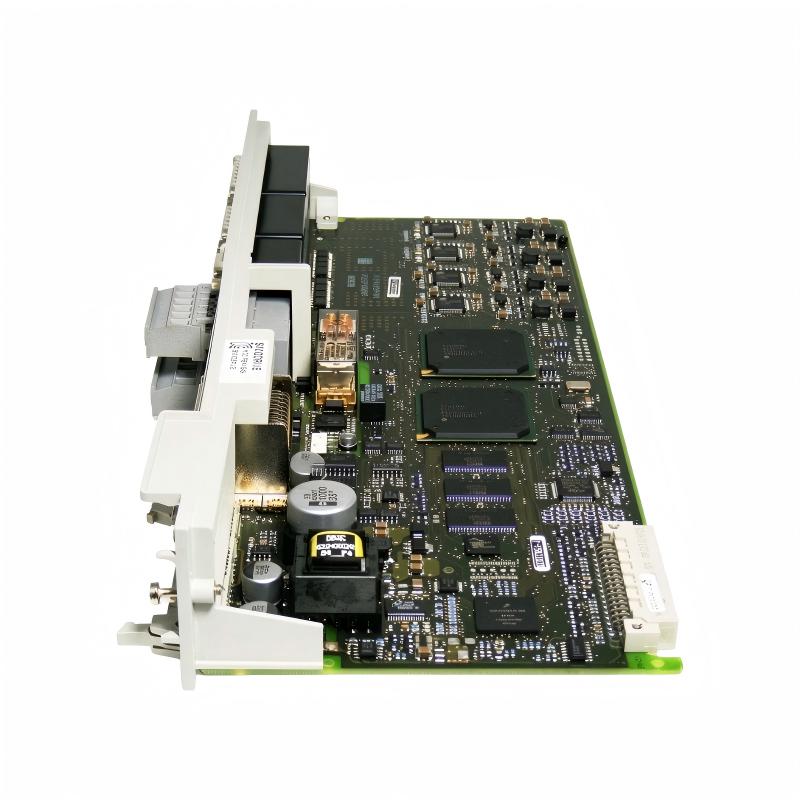
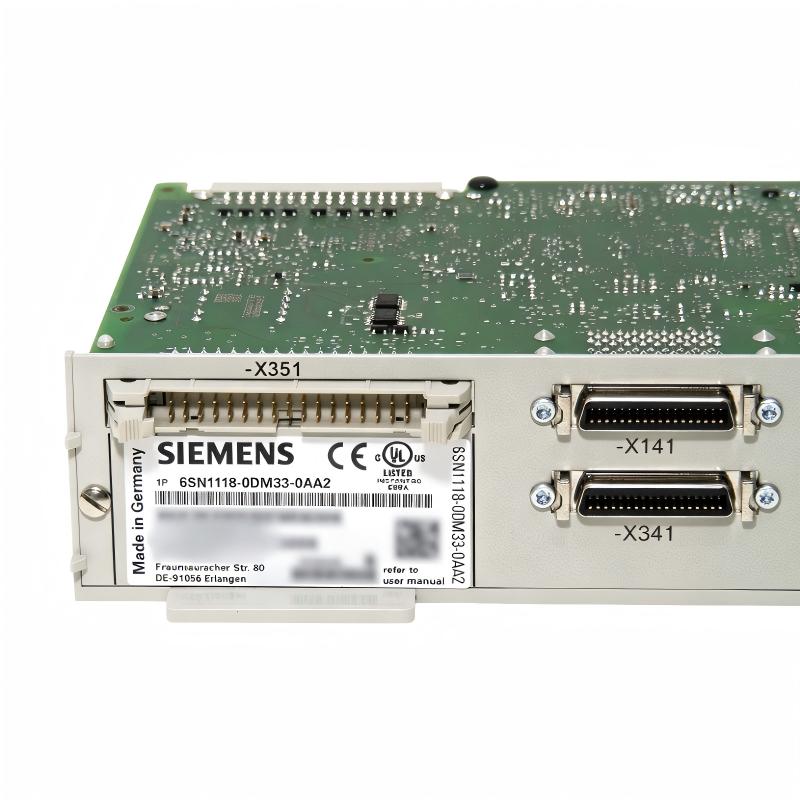
- Siemens
- 6SN1118-0DM33-0AA2
- Digital High Standard Closed-Loop Control Plug-In Unit
- Germany
- 318 × 44 × 127 mm
- 0.53 kg
- Xiamen, China
- New & In Stock
- T/T, PayPal, Western Union
- 1 Year
- 1-3 Working Days
- DHL, UPS, TNT, FedEx and EMS.
- 24-Hour Service
- COO
- 7
Our advantage
Global Logistics
We have a 10-year logistics and express cooperation agreement, so our products can be shipped to any place in the world.
Brand new and original
Our products are imported in bulk from the place of origin. Because of the cooperative relationship, our products are all original and 100% new.
24-hour service
We provide 7*24 hours service to our customers. We will be there whenever you need us.
Price advantage
All our products are priced very favorably because we have our own warehouse and supply.
| Company Information | |||
| [email protected] | |||
| Mobile | +8615980777398 | ||
| +8615980777398 | |||
| 15980777398 |
Product Overview
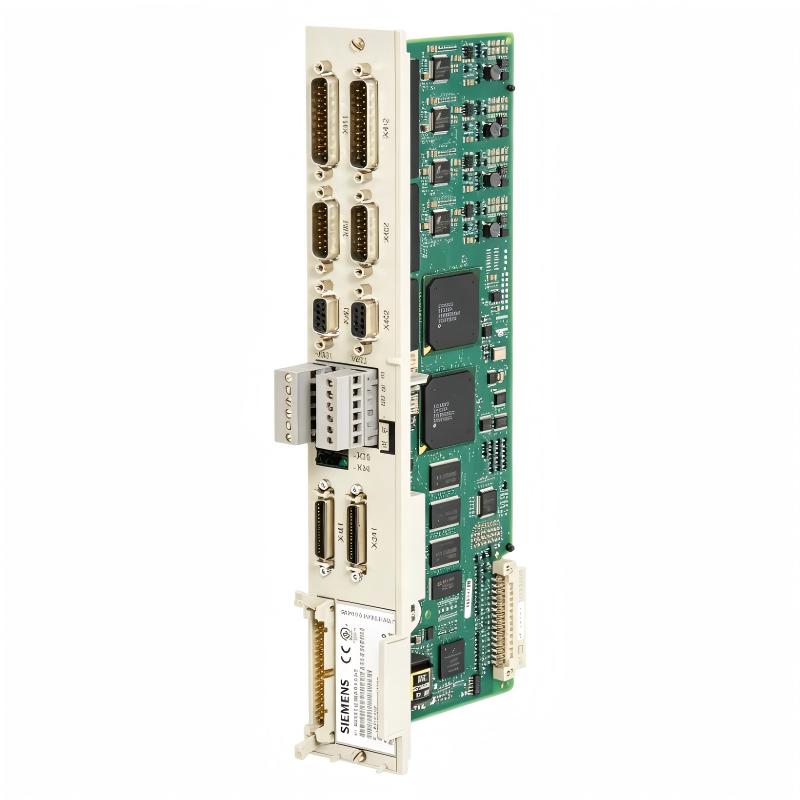
The Siemens 6SN1118-0DM33-0AA2 is a SIMODRIVE 611 Digital High Standard closed-loop control plug-in unit for two-axis CNC drive applications. It supports SIN/COS encoders with 1 Vpp signals and a digital speed/torque setpoint interface for compatible feed-drive and main-spindle configurations. The DM33 configuration also supports a direct measuring system, allowing the drive system to use position feedback measured at the machine axis. <Cite refs={[“turn675121search21″,”turn675121search8”]}/>
This feedback arrangement is useful in machine tools where motor rotation does not always translate directly into the expected axis movement. A ball-screw mechanism, coupling, or other transmission component can introduce mechanical clearance or positioning deviations. With a compatible direct measuring system, the control loop can use feedback from the actual measurement point rather than relying exclusively on motor encoder information.
Consider a CNC milling machine that needs to maintain accurate table positioning during repeated machining cycles. The CNC controller issues the movement commands, while the control unit processes feedback and coordinates the associated drive functions. If the machine uses direct axis measurement, the control system can account for measured movement at that point, although mechanical wear and incorrect feedback calibration still need to be addressed separately.
The 6SN1118-0DM33-0AA2 belongs to the High Standard control range, distinguishing it from related High Performance variants. Its two-axis designation does not mean that every combination of feed axes and main spindles is supported; the actual arrangement depends on the selected power modules, motors, feedback devices, and software configuration.
When replacing an installed unit, check the complete order number and the existing feedback arrangement. The DM33 variant supports direct measuring-system operation, so substituting a related control unit without the corresponding interface may require changes to the machine’s drive architecture.
Technical Specifications
| Parameter | Specification |
|---|---|
| Manufacturer | Siemens |
| Model | 6SN1118-0DM33-0AA2 |
| Product Family | SIMODRIVE 611 Digital |
| Product Type | Digital High Standard Closed-Loop Control Plug-In Unit |
| Control Classification | High Standard |
| Number of Axes | 2 |
| Encoder Compatibility | SIN/COS encoders, 1 Vpp |
| Setpoint Interface | Digital speed/torque setpoint interface |
| Direct Measuring System | Supported |
| Drive Applications | Feed Drive (FD) and Main Spindle Drive (MSD), subject to configuration |
| NC Software Requirement | Version 06.04.09 or later |
| Installation Type | Plug-in control unit |
| Compatible System | SIMODRIVE 611 Digital |
| Dimensions | 318 × 44 × 127 mm |
| Weight | 0.53 kg |
Product Features
- Two-axis closed-loop control: Supports the specified two-axis SIMODRIVE configuration.
- High Standard control classification: Identifies the unit’s control category within the SIMODRIVE 611 Digital range.
- Direct measuring-system support: Accommodates compatible feedback arrangements measuring movement at the machine axis.
- SIN/COS encoder interface: Supports the specified 1 Vpp encoder configuration.
- Digital speed/torque setpoint interface: Connects the control functions to compatible drive hardware.
- Feed-drive and spindle applications: Supports suitable axis configurations when matched with the corresponding motors and power modules.
- Software-dependent integration: Requires compatible NC software and correctly configured drive parameters.
Working Principle
The 6SN1118-0DM33-0AA2 processes motion commands and feedback within the SIMODRIVE 611 Digital drive system. The CNC controller requests movement, the associated power module supplies controlled electrical power to the motor, and the control unit uses the configured feedback signals to regulate the drive response.
A simplified control arrangement is:
CNC Controller → 6SN1118-0DM33-0AA2 → SIMODRIVE Power Module → Motor → Machine Axis
Direct Measuring System / Compatible Encoder → Feedback Interface → Closed-Loop Control
During a machining cycle, the control system compares the commanded movement with the available feedback and adjusts drive operation accordingly. The direct measuring-system capability is particularly relevant when actual machine-axis position needs to be measured independently of motor rotation.
For example, a motor may rotate through the expected angle while mechanical clearance in a ball-screw assembly causes the table to move differently from the commanded position. A suitably configured direct measuring system can report the movement at the selected axis measurement point, allowing the control loop to respond to the measured position. It does not, however, eliminate backlash or repair worn mechanical components.
Correct feedback configuration is essential. The measuring device, signal interface, scaling, axis assignment, and drive parameters must match the installed hardware. Incorrect settings can produce positioning errors even when the control unit and measuring device are individually functional.
During commissioning, verify the feedback signal and axis response under the machine’s approved test procedure. If the measured position differs from the expected movement, investigate the feedback wiring, measuring-system alignment, mechanical transmission, and parameter configuration before identifying the control unit as the cause.
Role in the SIMODRIVE 611 CNC Drive Architecture
The 6SN1118-0DM33-0AA2 occupies the closed-loop control position within a modular CNC drive system. It processes the configured motion commands and feedback signals while the CNC controller, power modules, motors, and measuring devices perform their respective functions.
CNC Controller → High Standard Control Unit → Power Module → Motor → Machine Axis
| System Element | Function |
|---|---|
| CNC Controller | Generates motion commands and coordinates machining sequences |
| 6SN1118-0DM33-0AA2 | Processes the specified two-axis closed-loop control functions |
| SIMODRIVE 611 Power Module | Supplies controlled electrical power to compatible motors |
| Feed Motor or Main-Spindle Motor | Produces the mechanical movement required by the machine |
| Direct Measuring System | Measures position at the configured machine-axis measurement point |
| Compatible SIN/COS Encoder | Supplies supported 1 Vpp feedback signals |
| Mechanical Transmission | Transfers motor movement to the machine axis |
| NC Software | Provides the required CNC and drive-control functions |
| Drive Parameters | Define axis behavior, feedback scaling, and control settings |
| CNC Electrical Cabinet | Houses the control and drive hardware |
Industrial Applications
| Application | Practical Use |
|---|---|
| CNC Milling Machines | Controlling feed-axis movement where direct position feedback is required |
| CNC Machining Centers | Coordinating axis movement during programmed machining cycles |
| CNC Turning Machines | Supporting compatible feed-drive and spindle-control arrangements |
| Precision Machine Tools | Using direct measuring-system feedback to assess actual axis position |
| Ball-Screw Feed Systems | Monitoring movement where motor rotation and table position may differ |
| Metalworking Production Equipment | Integrating closed-loop control into SIMODRIVE-based machinery |
| CNC Retrofit Projects | Replacing a control unit where the existing feedback architecture matches |
| Multi-Axis Machine Tools | Serving as a control component within a larger coordinated drive system |
Installation and Maintenance
- Verify the complete order number: Confirm 6SN1118-0DM33-0AA2 and distinguish it from related DM31 or High Performance variants.
- Check the axis arrangement: Confirm that the intended feed-drive or main-spindle configuration is supported by the unit and associated drive hardware.
- Confirm feedback compatibility: Verify that the measuring device and encoder interface match the specified SIN/COS 1 Vpp configuration and the installed system.
- Review direct measuring-system requirements: Determine where axis position is measured and confirm that the feedback arrangement matches the DM33 configuration.
- Check the drive assembly: Verify compatibility with the installed SIMODRIVE 611 power modules, motors, and control hardware.
- Isolate the equipment: Follow the approved shutdown, electrical isolation, and DC-link discharge procedures before accessing the drive system.
- Inspect feedback wiring: Check cables and connectors for loose contacts, damaged insulation, contamination, or incorrect pin assignments.
- Verify NC software compatibility: Confirm that the installed software meets the required version and supports the intended drive configuration.
- Back up existing parameters: Preserve axis assignments, feedback scaling, and control settings before replacing the unit.
- Check feedback direction and scaling: Confirm that measured movement corresponds to the expected axis direction and engineering units.
- Commission the axis under controlled conditions: Follow the machine’s commissioning procedure and verify the feedback response before returning the equipment to production.
- Record the final configuration: Document the control-unit reference, software version, measuring-system type, axis assignment, and commissioning results.
Compatible System Components
| Component | Function |
|---|---|
| Siemens 6SN1118-0DM33-0AA2 | Provides the specified two-axis High Standard closed-loop control configuration |
| SIMODRIVE 611 Power Modules | Supply controlled power to compatible motors |
| CNC Controller | Generates motion commands and coordinates machine operation |
| Compatible Feed Motors | Produce movement for configured feed axes |
| Compatible Main-Spindle Motors | Support spindle operation in suitable drive configurations |
| Direct Measuring System | Supplies machine-axis position feedback |
| SIN/COS 1 Vpp Encoders | Provide compatible encoder feedback |
| NC Software | Supplies the required CNC and drive-control functions |
| Drive Parameter Configuration | Defines axis behavior, feedback scaling, and control settings |
| CNC Electrical Cabinet | Houses the control unit and associated drive equipment |
Recommended Related Models
| Model | Product Type | Typical Application |
|---|---|---|
| Siemens 6SN1118-0DM33-0AA0 | Digital High Standard Closed-Loop Control Plug-In Unit | Comparing the same control family with a different order-code version |
| Siemens 6SN1118-0DM33-0AA1 | Digital High Standard Closed-Loop Control Unit | Evaluating the preceding order-code version for a compatible system |
| Siemens 6SN1118-0DM31-0AA2 | 2-Axis Digital High Standard Control Unit | Applications that do not require the DM33 direct measuring-system configuration |
| Siemens 6SN1118-0DM31-0AA0 | 2-Axis Digital High Standard Control Unit | Comparing the related High Standard configuration without direct measuring-system support |
| Siemens 6SN1118-0DK23-0AA2 | Digital High Performance Closed-Loop Control Unit | Applications requiring the specified High Performance configuration |
| Siemens 6SN1118-0DK21-0AA2 | Digital High Performance Closed-Loop Control Unit | Evaluating a related two-axis High Performance control configuration |
Key Advantages
- Supports two-axis closed-loop control within the SIMODRIVE 611 Digital system.
- Accommodates compatible direct measuring-system feedback.
- Supports SIN/COS 1 Vpp encoder arrangements.
- Integrates with compatible CNC controllers, power modules, and motors.
- Allows the feedback architecture to account for measured machine-axis movement.
Technical FAQs
How does the DM33 configuration differ from the DM31 control unit?
The DM33 configuration supports a direct measuring system, while the DM31 variant is intended for a different feedback arrangement without that direct measuring-system capability. Check the machine’s actual feedback architecture before selecting a replacement.
What encoder interface is specified for the 6SN1118-0DM33-0AA2?
The unit is specified for compatible SIN/COS encoders with 1 Vpp signals. The complete measuring chain must match the signal interface, wiring, and configured drive parameters.
Why should the measuring-system location be considered when selecting this unit?
Feedback measured at the motor may not fully represent movement at the machine axis if the mechanical transmission introduces backlash or other deviations. A compatible direct measuring system can provide feedback from the selected axis measurement point.
What should be checked if positioning accuracy deteriorates after installation?
Check the measuring-system signal, feedback scaling, axis assignment, cable connections, and drive parameters. Also inspect the mechanical transmission for backlash, wear, or coupling movement that could cause actual axis position to differ from the expected position.