

ProductPRODUCT
Featured products
Contact Us
- Siemens
- 6AV2123-2JB03-0AX0
- SIMATIC HMI Basic Panel
- Germany
- 267 × 182 × 39.4 mm
- 1.383 kg
- Xiamen, China
- New & In Stock
- T/T, PayPal, Western Union
- 1 Year
- 1-3 Working Days
- DHL, UPS, TNT, FedEx and EMS.
- 24-Hour Service
- COO
- 4
Our advantage

Global Logistics
We have a 10-year logistics and express cooperation agreement, so our products can be shipped to any place in the world.

Brand new and original
Our products are imported in bulk from the place of origin. Because of the cooperative relationship, our products are all original and 100% new.

24-hour service
We provide 7*24 hours service to our customers. We will be there whenever you need us.

Price advantage
All our products are priced very favorably because we have our own warehouse and supply.
| Company Information | |||
| [email protected] | |||
| Mobile | +8615980777398 | ||
| +8615980777398 | |||
| 15980777398 |
Product Overview
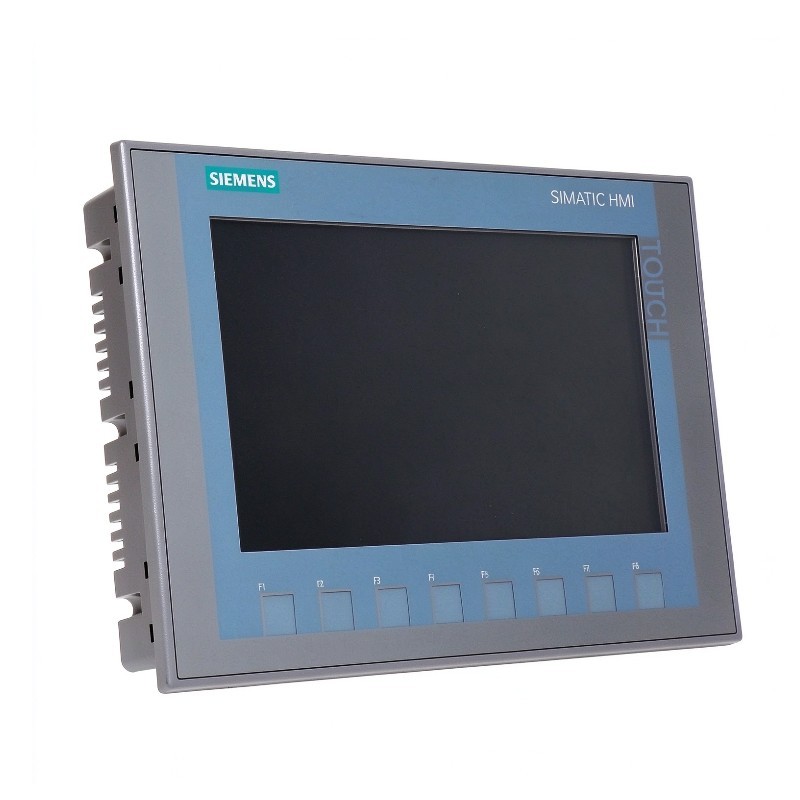
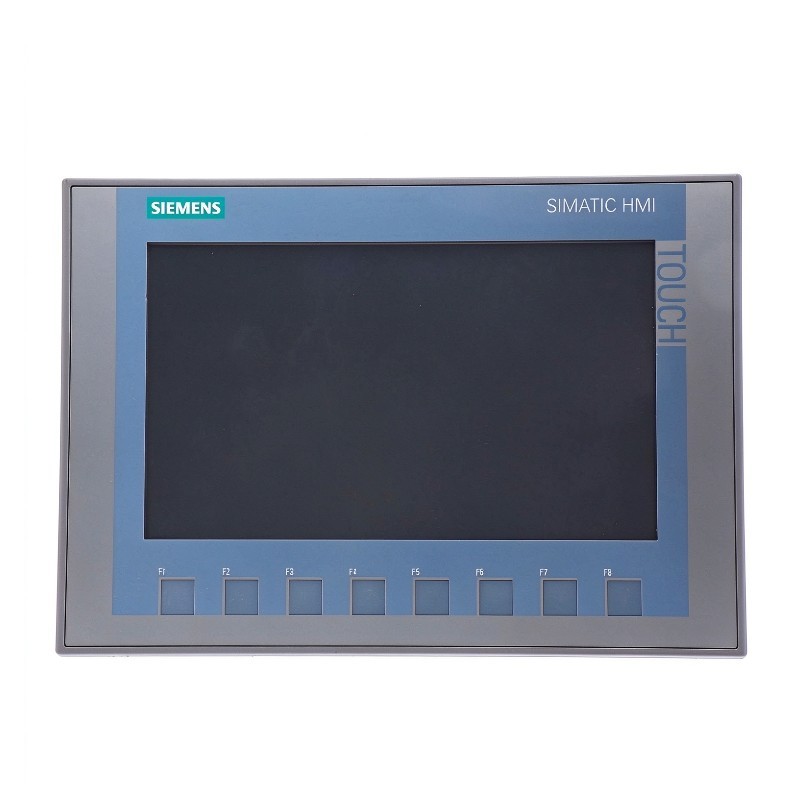
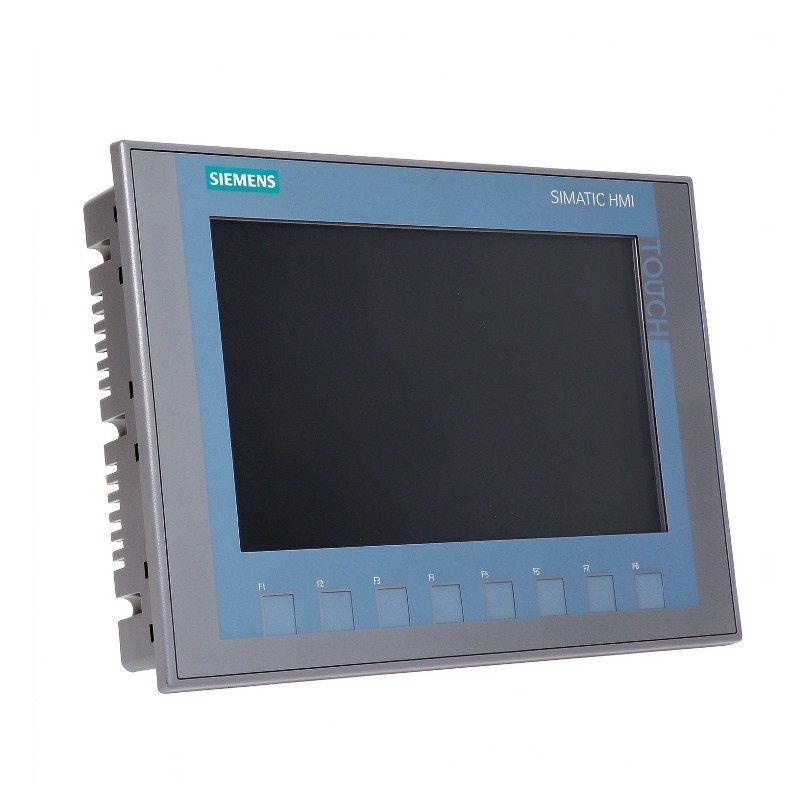
The Siemens 6AV2123-2JB03-0AX0 SIMATIC HMI Basic Panel is an industrial human-machine interface designed for machine operation, process visualization, and operator interaction with PLC-controlled equipment. Identified as the KTP900 Basic, this model combines a 9-inch TFT color display with touchscreen input and physical function keys. It provides a centralized interface for viewing machine conditions, accessing operating functions, and responding to process messages.
In an automated production environment, the operator interface must present useful information without requiring operators to work directly with PLC programming tools. The KTP900 Basic addresses this requirement through configurable screens that can display equipment states, process values, operating modes, alarms, and machine-specific controls. The layout and behavior of these screens are determined by the engineering project prepared for the application.
The 9-inch display supports 65,536 colors and an 800 × 480 pixel resolution. Its widescreen format accommodates multiple interface elements on a single screen, which can be useful when operators need to view several machine conditions together. Physical function keys complement touchscreen operation, allowing frequently used actions to be assigned to dedicated keys where appropriate.
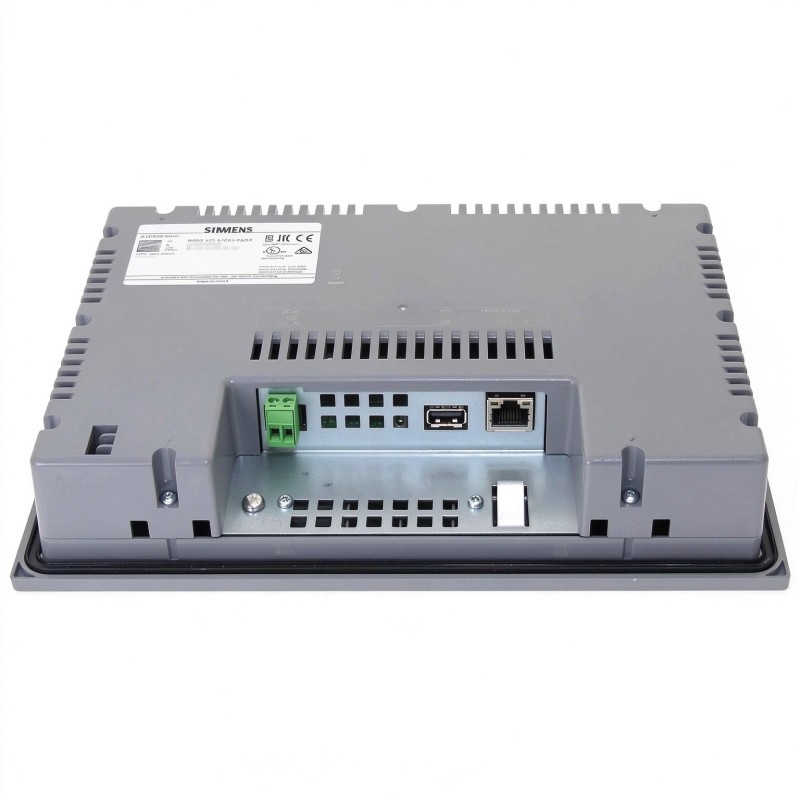
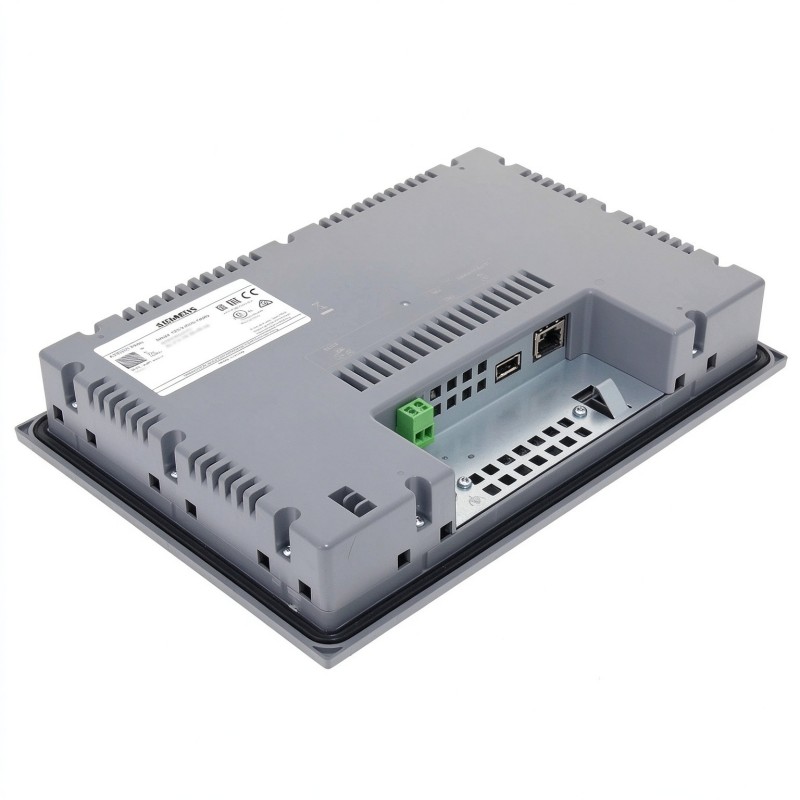
The 6AV2123-2JB03-0AX0 communicates with compatible automation equipment through its PROFINET interface. This supports integration into industrial Ethernet networks used by SIMATIC PLCs and other compatible controllers. The panel exchanges configured process data with the control system, allowing graphical objects to reflect PLC variables and operator inputs to be transferred to the relevant control logic.
Configuration is supported through WinCC Basic V13 or STEP 7 Basic V13. Within the engineering project, the machine designer establishes screen navigation, tag connections, numerical input fields, alarm presentation, and the behavior of operator controls. These settings determine how the HMI supports the machine’s operating procedures.
For example, a production machine may use separate screens for automatic operation, manual adjustments, fault messages, and maintenance information. Operators can move between these screens to review machine status or enter permitted operating values. The panel itself does not determine the production sequence; the PLC program and its associated field devices remain responsible for executing the control process.
The KTP900 Basic is suitable for machine-level visualization where a larger operator interface is useful for presenting multiple process variables or organizing more detailed screen layouts. Typical applications include packaging machinery, assembly equipment, production lines, material-handling systems, and industrial processing equipment.
A successful installation requires correct PROFINET configuration, accurate PLC tag assignments, and a properly engineered HMI project. The panel’s operating functions should be tested against the actual machine sequence, particularly where screen commands initiate changes to equipment states or operating parameters.
The Siemens 6AV2123-2JB03-0AX0 SIMATIC HMI Basic Panel combines graphical visualization, physical operator input, and industrial network communication in one terminal. It provides a configurable local interface for monitoring and operating compatible automation systems.
Technical Specifications
| Parameter | Specification |
|---|---|
| Manufacturer | Siemens |
| Model | 6AV2123-2JB03-0AX0 |
| Product Family | SIMATIC HMI Basic Panels, second generation |
| Product Type | KTP900 Basic |
| Display Type | TFT color display |
| Display Size | 9 inches |
| Display Resolution | 800 × 480 pixels |
| Number of Display Colors | 65,536 |
| Operator Control | Key and touch operation |
| Communication Interface | PROFINET |
| Engineering Software | WinCC Basic V13 / STEP 7 Basic V13 |
| Primary Function | Industrial machine operation and process visualization |
| Application Category | Human-machine interface |
| Dimensions | 267 × 182 × 39.4 mm |
| Weight | 1.383 kg |
Product Features
- 9-inch TFT color display: Presents machine status, process values, configured alarms, and operator controls on a widescreen interface.
- Key and touch operation: Combines touchscreen interaction with physical function keys for application-specific operator tasks.
- PROFINET communication: Exchanges configured data with compatible PLCs and automation devices over an industrial Ethernet network.
- 65,536 display colors: Supports clear visual differentiation between interface objects, operating states, and configured messages.
- Configurable screen layouts: Allows the interface to be organized around machine sequences, operating modes, and diagnostic requirements.
- PLC tag integration: Connects graphical objects and input fields to controller variables through the engineering project.
- SIMATIC engineering compatibility: Supports configuration with the specified WinCC Basic V13 or STEP 7 Basic V13 environment.
- Operator alarm display: Presents configured fault and status messages to help operators identify abnormal operating conditions.
- Dedicated physical controls: Allows selected functions to be assigned to physical keys where required by the machine workflow.
- Machine-level visualization: Consolidates operating information and authorized commands into a local operator station.
Working Principle
The Siemens 6AV2123-2JB03-0AX0 operates as the human-machine interface within a compatible PLC-based automation system. It receives configured process information from the controller, displays that information through its graphical interface, and transfers operator inputs through PROFINET.
Operator Input → HMI Application → PROFINET Communication → PLC Logic → Machine Response
The operating process begins with the HMI project created in the engineering environment. The project defines the screens, navigation paths, process tags, graphical objects, and command behavior. After the project is transferred to the panel, these settings determine what the operator sees and how the interface responds to input.
During normal operation, the HMI exchanges configured data with the PLC through PROFINET. Each connected screen object uses its assigned tag to display or interact with a controller variable. A status indicator might show whether a motor is running, while a numerical field could display a pressure reading, temperature, counter, or production value.
When an operator touches a configured control or presses an assigned physical key, the HMI processes the input according to the application. If the action is linked to a PLC variable or command, the corresponding data is transmitted to the controller. The PLC program then evaluates the request and determines the machine response according to its operating logic and interlocks.
The display is updated as the controller’s data changes. This feedback allows operators to observe equipment states and determine whether a requested operation has taken effect. Configured alarm messages can also present information about faults or abnormal process conditions identified by the automation system.
The physical function keys provide a direct input method for selected operations. Their assignments depend on the engineering project and should be tested during commissioning. Appropriate assignments help ensure that common tasks can be performed consistently without requiring operators to navigate through multiple screens.
PROFINET configuration is essential to this process. The panel, controller, and network must use compatible communication settings, and the HMI project must reference the correct PLC variables. A network connection alone does not guarantee that the application is functioning correctly if tag assignments or command mappings are incorrect.
The panel does not independently execute the machine’s PLC control program. It supplies the operator-facing interface, while the controller manages process logic and communicates with field devices. Essential interlocks and machine-protection functions must be implemented within the appropriate control architecture.
Once the HMI project and communication connection have been commissioned, the KTP900 Basic provides operators with a local view of machine operation and a configured means of interacting with the control system. Its effectiveness depends on accurate engineering, correct data mapping, and appropriate screen design.
Role in the Industrial Control Architecture
The 6AV2123-2JB03-0AX0 occupies the operator-interface layer of a compatible SIMATIC automation system. It presents process information from the controller and forwards configured operator inputs over PROFINET.
Operator → KTP900 Basic HMI → PROFINET Network → PLC → Field Devices
| System Component | Function |
|---|---|
| Siemens KTP900 Basic HMI | Displays process information and accepts configured operator commands |
| SIMATIC PLC | Executes the automation program and manages machine behavior |
| PROFINET Network | Transfers configured data between compatible automation devices |
| PLC Digital Input Modules | Acquire discrete signals from sensors and switches |
| PLC Digital Output Modules | Provide control signals to connected equipment |
| PLC Analog Input Modules | Acquire analog process measurements |
| PLC Analog Output Modules | Supply analog reference signals where required |
| Sensors | Provide process measurements and equipment-state information |
| Motor Drives | Control motor operation according to the PLC program |
| Actuators | Carry out commands issued by the control system |
| Engineering Software | Defines HMI screens, tags, navigation, and communication settings |
The HMI provides the operator-facing visualization and input mechanism. The PLC and connected field devices execute the underlying control functions, while PROFINET carries the configured data needed for coordinated operation.
Industrial Applications
| Application | Typical Use |
|---|---|
| Packaging Machinery | Displaying production status, machine modes, and configured operating commands |
| Assembly Equipment | Presenting station conditions, process values, and operator instructions |
| Automated Production Lines | Monitoring equipment states and displaying configured alarms |
| Material-Handling Systems | Showing conveyor status and fault information |
| Industrial Processing Equipment | Visualizing process measurements and operating conditions |
| Manufacturing Machines | Providing local access to PLC-controlled functions |
| Pumping Systems | Displaying equipment status and selected process variables |
| Machine Tool Support Equipment | Presenting operating screens and diagnostic information |
| Production Utility Systems | Monitoring connected equipment through a local operator interface |
| Control Cabinet Installations | Providing a dedicated HMI for compatible automation systems |
Installation and Maintenance
- Confirm application compatibility: Ensure that the KTP900 Basic provides the required visualization functions and that PROFINET is suitable for the intended automation network.
- Prepare the mounting location: Check the enclosure opening, mounting arrangement, and environmental conditions against the equipment documentation.
- Inspect mounting hardware: Verify that the required mounting components are available and that the panel can be secured correctly.
- Verify the power supply: Confirm that the installation provides the specified DC supply within the permitted operating range.
- Connect the PROFINET network: Use appropriate industrial Ethernet cabling and follow the network topology specified for the control system.
- Prepare the HMI project: Configure the screens, navigation, process tags, alarm messages, and operator functions in the applicable engineering environment.
- Establish PLC communication: Check device addressing and connection settings, then confirm that the panel can exchange data with the intended controller.
- Validate tag assignments: Compare displayed values and input fields with the corresponding PLC variables to identify incorrect mappings.
- Test physical function keys: Verify the configured behavior of the physical keys and confirm that they do not initiate unintended machine operations.
- Check screens and alarms: Test screen navigation, process displays, alarm messages, and operating commands under representative conditions.
- Inspect the installed panel: Keep the front operating surface clean using an appropriate method and inspect the mounting arrangement and connections for damage.
- Maintain configuration records: Preserve the approved HMI project, communication settings, and relevant backup information for troubleshooting and future maintenance.
If communication problems occur, inspect the network cabling, controller status, device configuration, and PROFINET settings. If displayed values are incorrect, check the PLC tag mapping and application logic before assuming that the HMI hardware is defective.
Related Components
| Component | Function |
|---|---|
| Siemens 6AV2123-2JB03-0AX0 KTP900 Basic | Provides the local operator interface with PROFINET communication |
| SIMATIC PLC | Executes the control program and manages connected equipment |
| PROFINET Cable | Transfers data between the HMI, PLC, and compatible network devices |
| Industrial Ethernet Switch | Connects automation devices where required by the network topology |
| PLC Digital Input Module | Acquires discrete field signals |
| PLC Digital Output Module | Provides discrete control outputs |
| PLC Analog Input Module | Acquires analog process measurements |
| PLC Analog Output Module | Supplies analog reference signals where required |
| Motor Drive | Controls motor operation in compatible applications |
| Industrial DC Power Supply | Supplies electrical power to the panel and associated control equipment |
| HMI Engineering Software | Configures screen layouts, tags, alarms, and communication settings |
Recommended Related Models
| Model | Product Type | Typical Application |
|---|---|---|
| Siemens 6AV2123-2DB03-0AX0 | SIMATIC HMI KTP400 Basic | Compact operator interface with key/touch operation and PROFINET |
| Siemens 6AV2123-2GB03-0AX0 | SIMATIC HMI KTP700 Basic | 7-inch Basic Panel with key/touch operation and PROFINET |
| Siemens 6AV2123-2JB03-0AX0 | SIMATIC HMI KTP900 Basic | 9-inch Basic Panel with key/touch operation and PROFINET |
| Siemens 6AV2123-2MB03-0AX0 | SIMATIC HMI KTP1200 Basic | Larger-screen Basic Panel for compatible automation systems |
Key Advantages
- Combines touchscreen interaction and physical function keys in one operator interface.
- Presents PLC process values and machine states on a widescreen color display.
- Supports integration into compatible PROFINET-based automation networks.
- Allows screen layouts and operating workflows to be tailored to the application.
- Provides local access to configured alarm and diagnostic information.
- Supports machine monitoring and operator interaction through a dedicated HMI terminal.
Technical FAQs
What display capabilities does the KTP900 Basic offer for machine visualization?
The panel uses a 9-inch TFT display with 65,536 colors and an 800 × 480 pixel resolution. The available screen area can accommodate configured process values, status indicators, alarm messages, and operator controls.
How does the KTP900 Basic communicate with the PLC?
The panel uses PROFINET to exchange configured process data with compatible automation equipment. The HMI project defines the communication settings and tag assignments used to display controller variables and transmit operator inputs.
Can the panel display application-specific alarms and diagnostic messages?
Yes. Alarm and diagnostic presentation can be configured in the HMI project, provided that the required information is available from the controller or application logic. The displayed messages depend on the configured alarm definitions and data connections.
Does the HMI determine whether a machine command is safe to execute?
No. The HMI transmits configured operator inputs, but the PLC program and appropriate control architecture must determine whether an operation is permitted. Interlocks and essential protection functions should not depend solely on the HMI interface.