ProductPRODUCT
Featured products
Contact Us
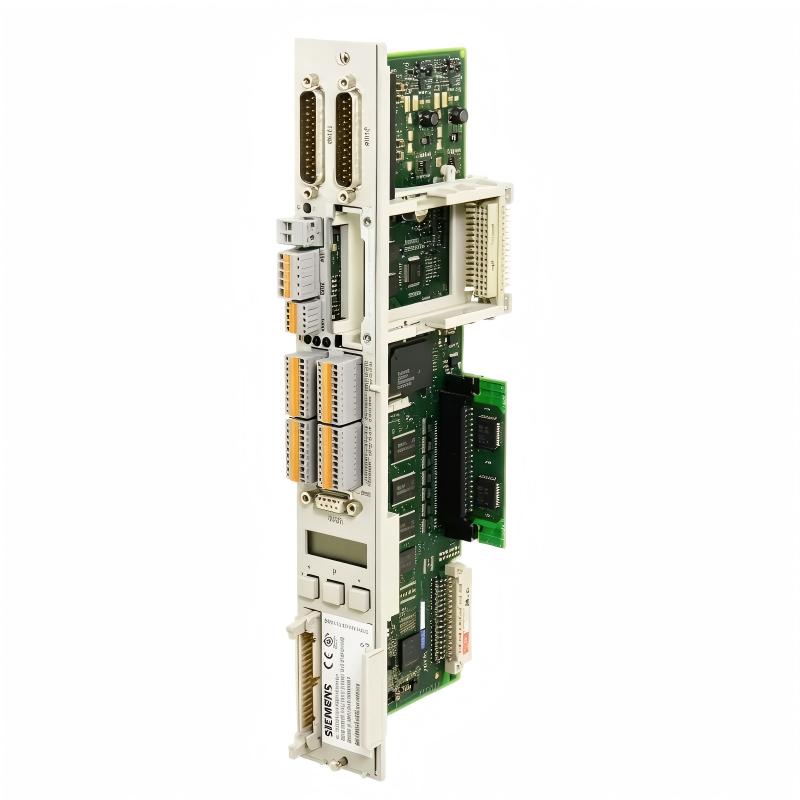
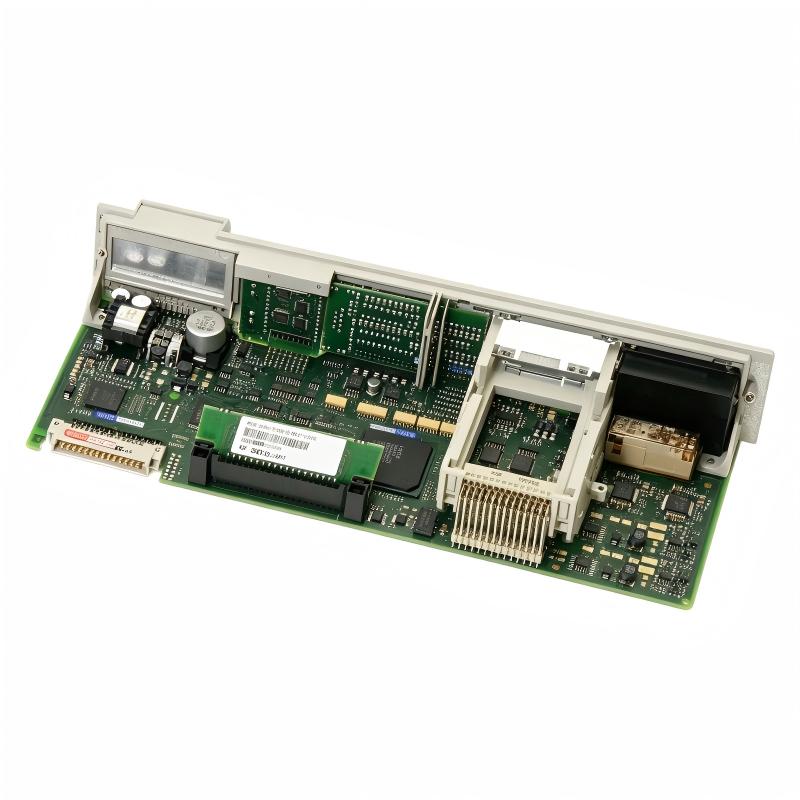
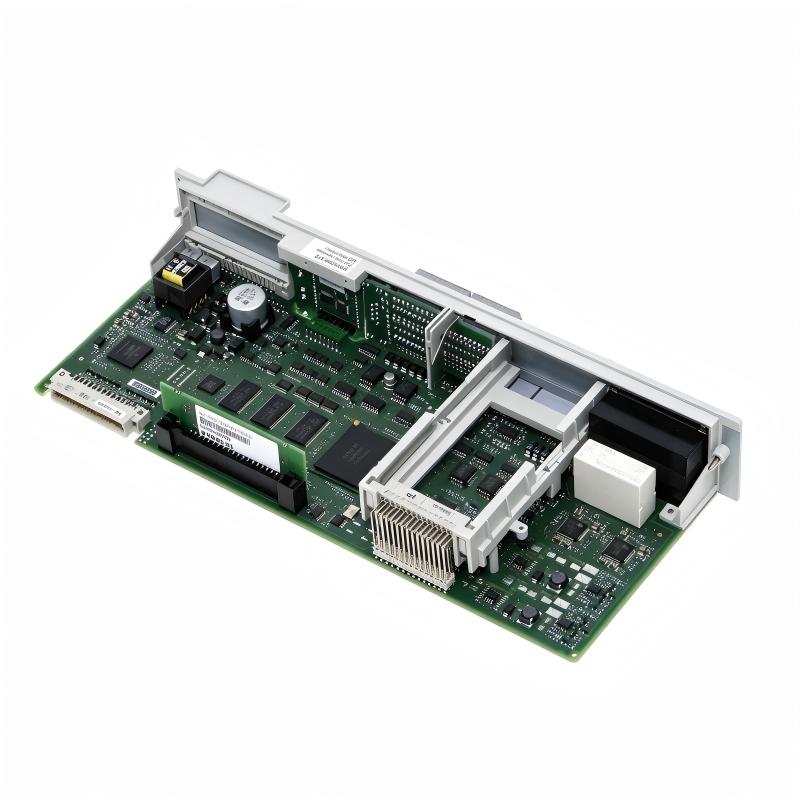
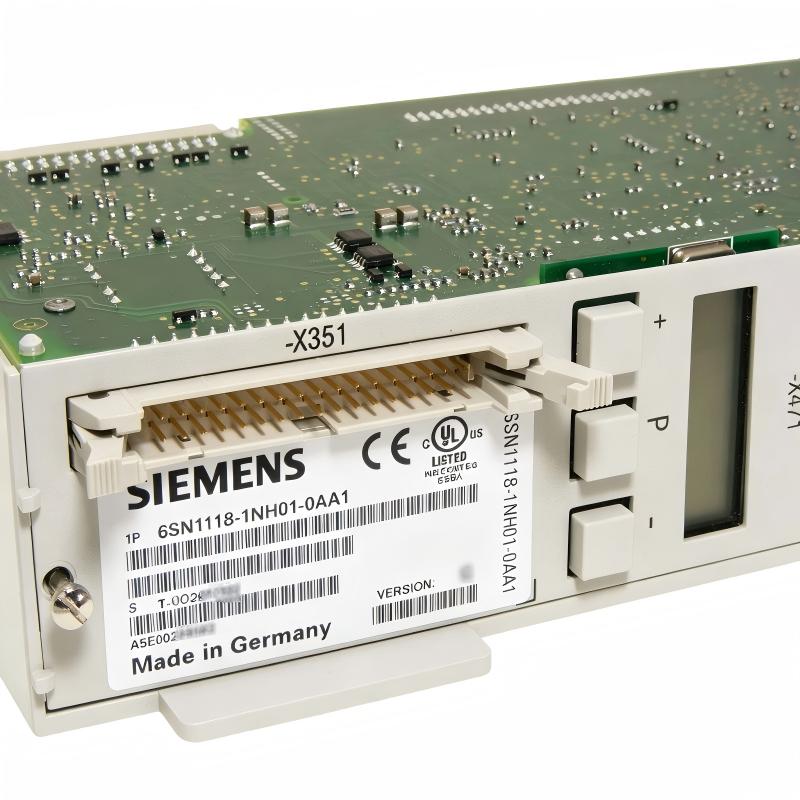
- Siemens
- 6SN1118-1NH01-0AA1
- 2-Axis Control-Loop Block
- Germany
- 330 × 51 × 152 mm
- 0.57 kg
- Xiamen, China
- New & In Stock
- T/T, PayPal, Western Union
- 1 Year
- 1-3 Working Days
- DHL, UPS, TNT, FedEx and EMS.
- 24-Hour Service
- COO
- 6
Our advantage
Global Logistics
We have a 10-year logistics and express cooperation agreement, so our products can be shipped to any place in the world.
Brand new and original
Our products are imported in bulk from the place of origin. Because of the cooperative relationship, our products are all original and 100% new.
24-hour service
We provide 7*24 hours service to our customers. We will be there whenever you need us.
Price advantage
All our products are priced very favorably because we have our own warehouse and supply.
| Company Information | |||
| [email protected] | |||
| Mobile | +8615980777398 | ||
| +8615980777398 | |||
| 15980777398 |
Product Overview
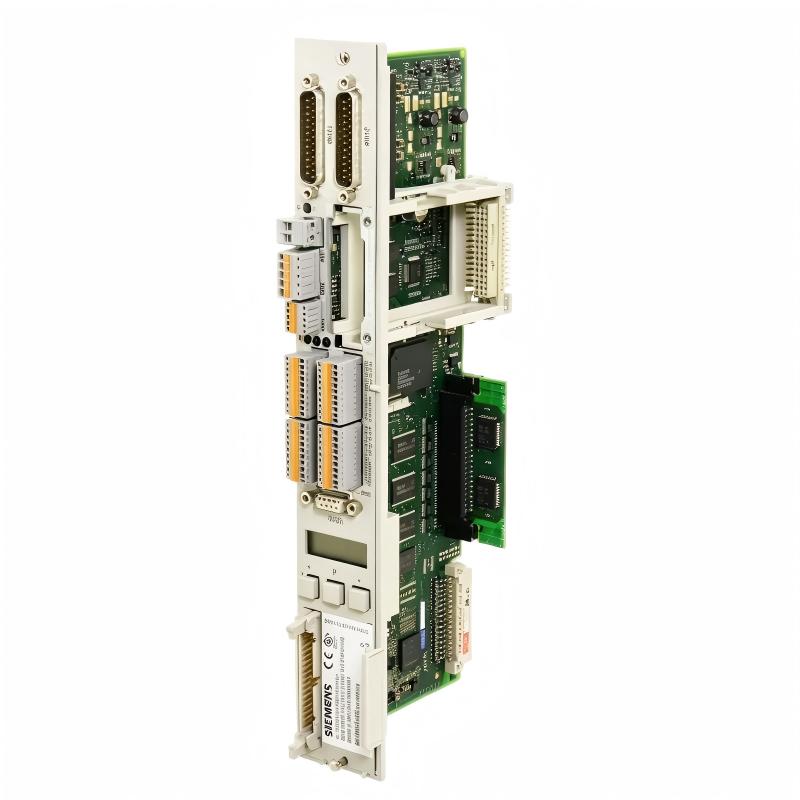
The Siemens 6SN1118-1NH01-0AA1 is a SIMODRIVE 611 universal HR two-axis control-loop block with positioning functionality. It supports compatible incremental encoders using sin/cos 1 Vpp signals and absolute encoders using supported EnDat interfaces. Within the SIMODRIVE drive architecture, the module processes motion commands and encoder feedback for two controlled axes.
In a CNC machine tool, two feed axes may need to follow programmed movements while maintaining accurate position feedback. This control-loop block handles the configured drive-control functions for both axes, working with the associated power modules to regulate motor operation. The machine controller coordinates the machining sequence, while the drive system manages the corresponding motor-control loops.
The 6SN1118-1NH01-0AA1 combines speed and torque setpoint control with positioning functionality. This distinguishes it from the related 6SN1118-0NH01-0AA1, which is configured for speed and torque setpoint control without the same positioning function. The distinction matters when selecting a replacement for an existing machine because the control requirements and parameter configuration must match.
The module can also be used in a suitable single-axis arrangement, even though it provides two drive-control channels. Its application depends on the connected motors, feedback interfaces, power modules, and the functions required by the machine controller.
Technical Specifications
| Parameter | Specification |
|---|---|
| Manufacturer | Siemens |
| Model / Article Number | 6SN1118-1NH01-0AA1 |
| Product Family | SIMODRIVE 611 universal HR |
| Product Type | 2-Axis Control-Loop Block |
| Number of Axes | 2 |
| Feedback Type | Incremental sin/cos 1 Vpp and supported absolute EnDat encoders |
| Control Functions | Speed, torque, and positioning |
| Drive System | SIMODRIVE 611 universal |
| Hardware Generation | HR |
| Expansion Capability | Compatible optional interface modules |
| Optional Interfaces | PROFIBUS DP and supported serial interfaces, depending on configuration |
| Compatible Motor Families | Selected 1FT6, 1FK, 1FE1, 1FW6, 2SP1, 1PH, 1PM6, and 1FN motor configurations |
| Dimensions | 330 × 51 × 152 mm |
| Weight | 0.57 kg |
Product Features
- Two-axis closed-loop control: Handles two drive-control channels within one SIMODRIVE control board.
- Positioning functionality: Supports positioning operations alongside speed and torque setpoint control.
- Sin/cos 1 Vpp encoder compatibility: Processes supported incremental encoder feedback for the connected axes.
- Absolute encoder support: Accommodates compatible EnDat feedback arrangements.
- Independent axis configuration: Allows each axis to use its assigned feedback signals and control parameters.
- SIMODRIVE 611 integration: Operates with compatible power modules and higher-level machine controllers.
- Optional interface expansion: Supports designated communication options where required by the machine configuration.
- Single-axis utilization: Can be used for one-axis operation when the overall drive arrangement permits it.
Working Principle
The 6SN1118-1NH01-0AA1 functions as the closed-loop control element for two compatible drive axes. It receives movement commands from the machine controller and processes encoder feedback to regulate the motors through their associated power modules.
A typical control arrangement follows this sequence:
Machine Controller → Position and Speed Commands → 6SN1118-1NH01-0AA1 → Power Modules → Motors
Motor Encoders → Feedback Signals → Control-Loop Block
During a positioning operation, the machine controller specifies the required movement. The control-loop block processes the configured command and feedback information, while the associated power module supplies the electrical power needed by the motor. The feedback loop allows the drive system to evaluate actual movement against the commanded operating condition.
For example, a CNC machine may use two feed axes to move a tool assembly and a workpiece table. Each axis has its own movement command, motor configuration, and feedback channel. The control-loop block manages the configured drive functions, while the machine controller coordinates both axes with the machining sequence.
Encoder compatibility is important to correct operation. Incremental sin/cos 1 Vpp signals and absolute EnDat signals use different feedback arrangements and initialization requirements. The selected control unit, motor encoder, cabling, and parameter configuration must be compatible with one another.
The control-loop block does not directly supply the motors’ main operating power. It relies on compatible SIMODRIVE 611 power modules, correctly connected feedback devices, and a properly configured machine-control interface.
Role in the SIMODRIVE 611 Control Architecture
The 6SN1118-1NH01-0AA1 occupies the drive-control layer between the higher-level machine controller and the power stages. It processes commands and feedback for two axes, while the power modules drive the motors and the machine controller coordinates the overall movement sequence.
Machine Controller → Position and Speed Commands → 6SN1118-1NH01-0AA1 → Power Modules → Motors
Motor Encoders → Feedback Connections → Control-Loop Block
| System Component | Function |
|---|---|
| 6SN1118-1NH01-0AA1 | Provides two-axis closed-loop control with positioning functionality |
| SIMODRIVE 611 Power Modules | Supply the connected motors |
| Compatible Siemens Motors | Produce the required mechanical movement |
| Incremental Encoders | Provide supported sin/cos 1 Vpp feedback |
| Absolute EnDat Encoders | Supply absolute-position information where supported |
| Machine Controller | Coordinates axis commands and machine sequences |
| Encoder Feedback Cables | Carry feedback signals to the control unit |
| Motor Power Cables | Connect motors to their associated power stages |
| TERMINALS Option Module | Provides supported terminal-interface functionality |
| PROFIBUS DP Option Module | Adds compatible fieldbus communication where configured |
Industrial Applications
| Application | Typical Use |
|---|---|
| CNC Machine Tools | Controlling two positioning-capable feed axes |
| Machine-Tool Feed Drives | Coordinating tool and workpiece movement |
| Industrial Positioning Systems | Regulating two motor-driven axes |
| Metalworking Machinery | Controlling feed movements during machining |
| Automated Production Equipment | Integrating two controlled axes into a machine sequence |
| Material Processing Systems | Coordinating motorized positioning mechanisms |
| Industrial Motion-Control Cabinets | Providing two-axis closed-loop drive control |
| Machine Rebuilding Projects | Replacing a control board after encoder and firmware checks |
| Existing SIMODRIVE Installations | Maintaining compatible positioning configurations |
| Multi-Axis Machinery | Managing two axes within a wider machine-control architecture |
Installation and Maintenance
- Verify the complete order number: Confirm 6SN1118-1NH01-0AA1 and distinguish it from the related speed/torque-only version.
- Check the drive-system configuration: Verify that the installed SIMODRIVE 611 system supports the control-loop block and its hardware generation.
- Identify both encoder types: Confirm whether each motor uses a compatible incremental sin/cos 1 Vpp encoder or an absolute EnDat encoder.
- Confirm power-module compatibility: Check that the associated power stages match the connected motors and intended operating requirements.
- Isolate the equipment: Follow the approved electrical safety procedure and verify that hazardous energy has been removed before accessing the drive system.
- Inspect feedback wiring: Check encoder cables, connectors, shielding, and channel assignments for damage or incorrect connections.
- Review optional interfaces: Confirm whether the installation requires a TERMINALS or PROFIBUS DP option and verify its compatibility.
- Verify motor and encoder parameters: Check motor data, feedback scaling, encoder configuration, and control settings for both axes.
- Check positioning parameters: Confirm that the required positioning functions and machine-controller commands are configured correctly.
- Test feedback channels: During controlled commissioning, verify that each encoder signal corresponds to the intended motor and axis.
- Investigate positioning errors: Check feedback signals, axis assignments, motor parameters, mechanical transmission, and control settings if actual movement differs from the command.
- Document the final configuration: Record the control-loop block reference, encoder types, motor assignments, option modules, parameter settings, and commissioning results.
Compatible System Components
| Component | Function |
|---|---|
| Siemens SIMODRIVE 611 Power Modules | Supply electrical power to the connected motors |
| Compatible Siemens Motors | Provide mechanical movement for each controlled axis |
| Compatible sin/cos 1 Vpp Encoders | Provide incremental position feedback |
| Compatible EnDat Absolute Encoders | Supply absolute-position feedback where supported |
| Encoder Feedback Cables | Connect encoder signals to the control unit |
| Motor Power Cables | Connect the motors to their associated power stages |
| Higher-Level Machine Controller | Generates movement commands and coordinates machine operation |
| Siemens 6SN1114-0NA00-0AA0 TERMINALS Option | Provides supported terminal-interface functionality |
| Siemens 6SN1114-0NB00-0AA2 PROFIBUS DP2 Option | Adds compatible PROFIBUS communication functionality |
| SIMODRIVE Commissioning Tools | Support parameterization and drive testing |
Recommended Related Models
| Model | Product Type | Typical Application |
|---|---|---|
| Siemens 6SN1118-1NH01-0AA1 | 2-Axis Control-Loop Block | Two-axis positioning with compatible encoder feedback |
| Siemens 6SN1118-0NH01-0AA1 | 2-Axis Closed-Loop Control Unit | Two-axis speed/torque setpoint control |
| Siemens 6SN1118-1NH01-0AA0 | 2-Axis Closed-Loop Control Unit | Related positioning-capable control configuration |
| Siemens 6SN1118-1NJ01-0AA1 | 1-Axis Positioning Control Module | Single-axis positioning using resolver feedback |
| Siemens 6SN1118-1NK01-0AA1 | 2-Axis Positioning Control Module | Two-axis positioning using resolver feedback |
| Siemens 6SN1114-0NB00-0AA2 | PROFIBUS DP2 Option Module | Adding supported PROFIBUS communication functionality |
Key Advantages
- Provides two-axis closed-loop control within the SIMODRIVE 611 system.
- Supports positioning in addition to speed and torque setpoint control.
- Accommodates compatible incremental and absolute encoder configurations.
- Allows independent feedback and parameter settings for two axes.
- Supports optional interface expansion where required.
- Integrates with compatible power modules and higher-level machine controllers.
Technical FAQs
What distinguishes the 6SN1118-1NH01-0AA1 from the 6SN1118-0NH01-0AA1?
The 6SN1118-1NH01-0AA1 includes positioning functionality, whereas the 6SN1118-0NH01-0AA1 is the speed/torque setpoint version. The choice depends on the control functions required by the machine.
Which feedback signals must the connected motors provide?
The module supports compatible incremental encoders using sin/cos 1 Vpp signals and supported absolute encoder configurations using EnDat. The motor encoder, cable arrangement, and control-unit configuration must match.
Can this control-loop block operate with only one active axis?
Yes. The SIMODRIVE 611 universal HR architecture permits two-axis control boards to be used in suitable single-axis applications. The connected power module, motor feedback, and configuration must still be appropriate.
What should be investigated if the position feedback appears correct but the axis stops at the wrong location?
Check the positioning parameters, command scaling, axis assignment, reference or initialization procedure, and mechanical transmission. Confirm that the machine controller and drive use consistent units and coordinate settings.