

ProductPRODUCT
Featured products
Contact Us
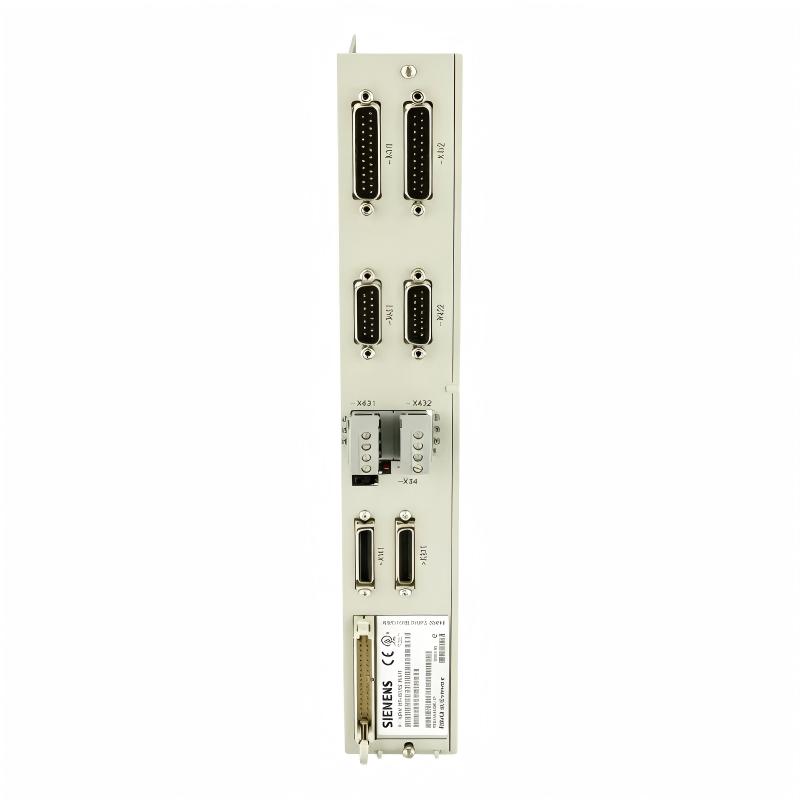
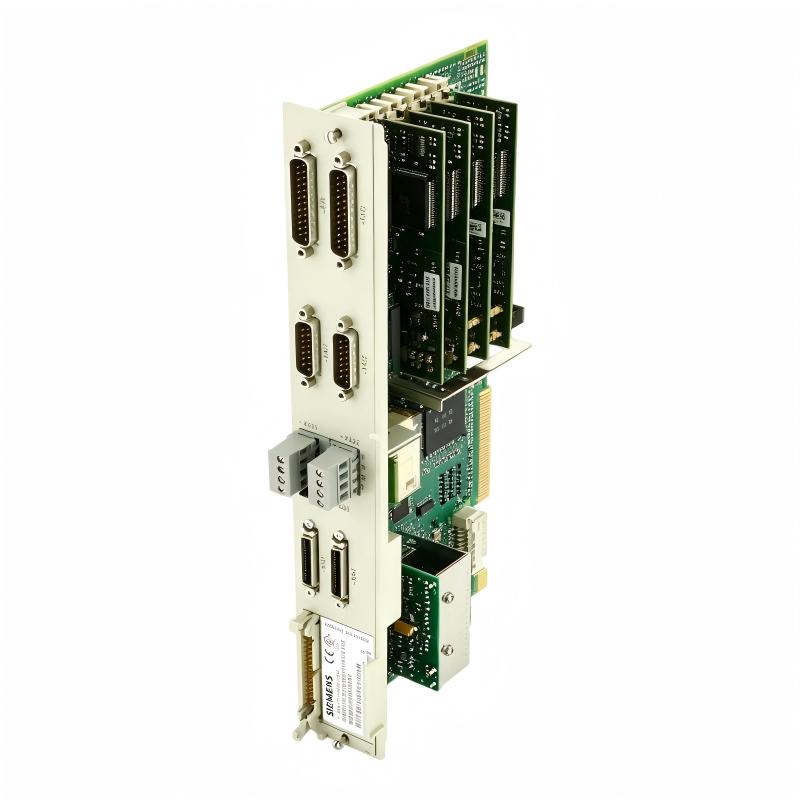
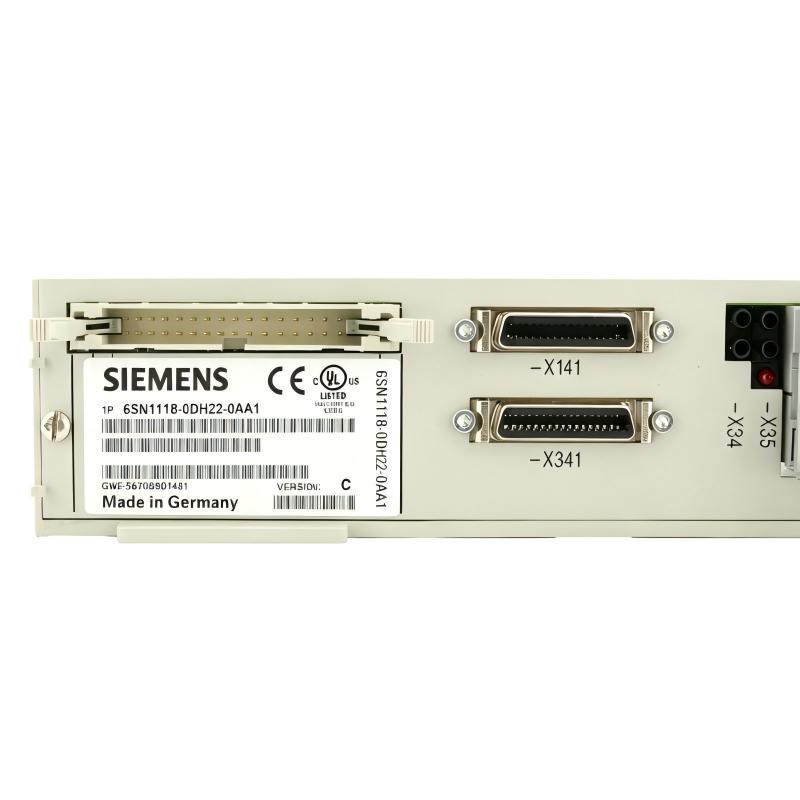
- Siemens
- 6SN1118-0DH22-0AA1
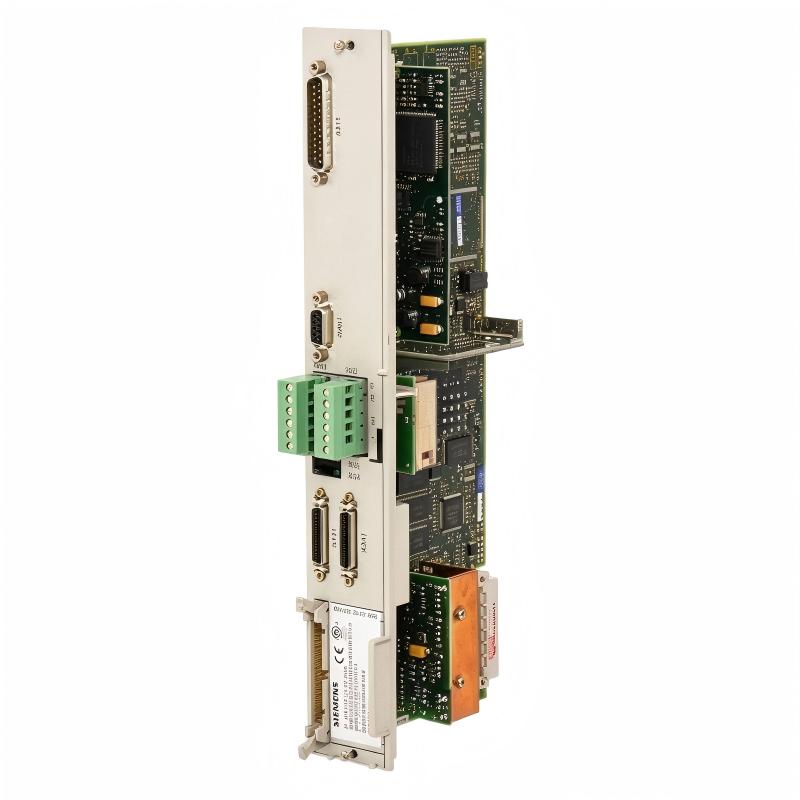
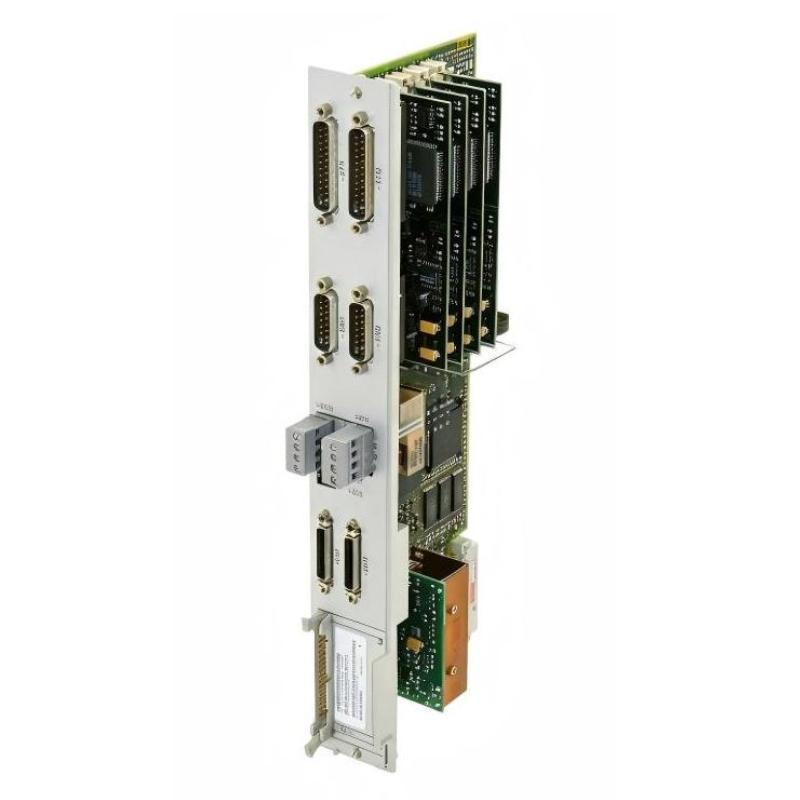
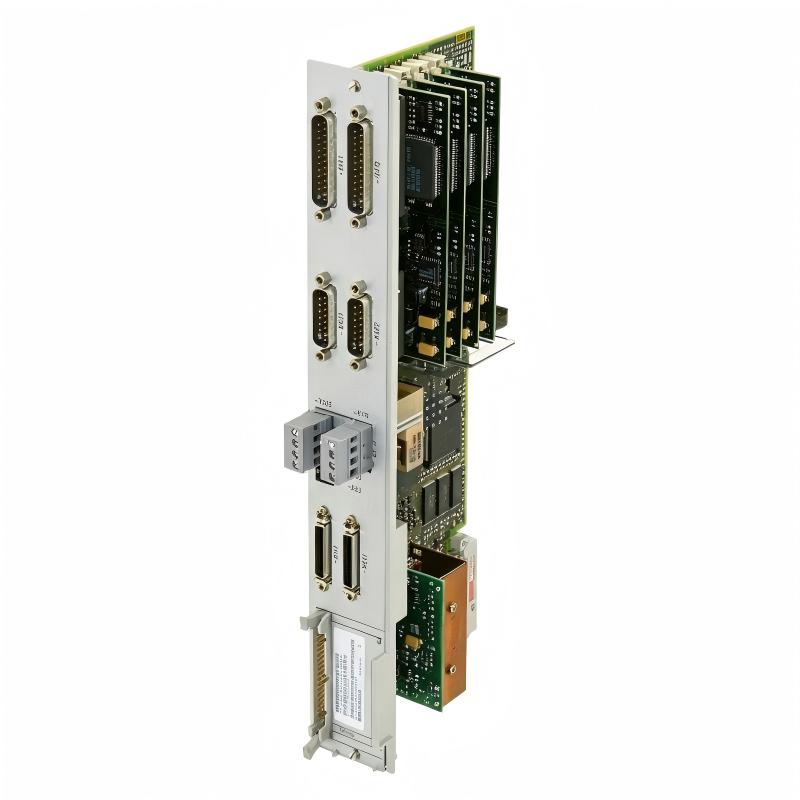
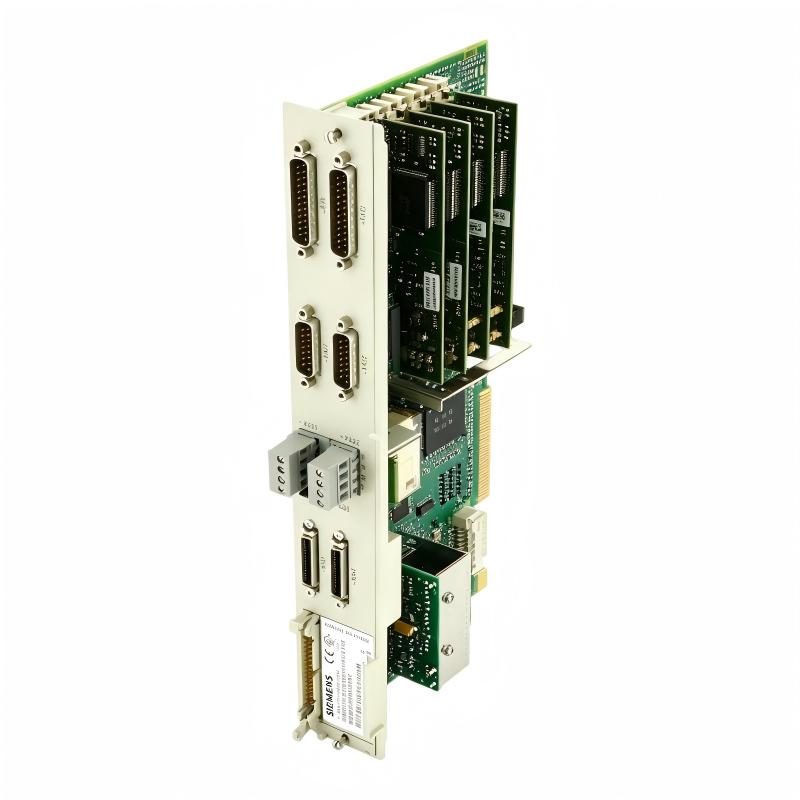
- Closed-Loop Plug-In Performance Control Unit
- Germany
- 330 × 51 × 152 mm
- 0.84 kg
- Xiamen, China
- New & In Stock
- T/T, PayPal, Western Union
- 1 Year
- 1-3 Working Days
- DHL, UPS, TNT, FedEx and EMS.
- 24-Hour Service
- COO
- 4
Our advantage

Global Logistics
We have a 10-year logistics and express cooperation agreement, so our products can be shipped to any place in the world.

Brand new and original
Our products are imported in bulk from the place of origin. Because of the cooperative relationship, our products are all original and 100% new.

24-hour service
We provide 7*24 hours service to our customers. We will be there whenever you need us.

Price advantage
All our products are priced very favorably because we have our own warehouse and supply.
| Company Information | |||
| [email protected] | |||
| Mobile | +8615980777398 | ||
| +8615980777398 | |||
| 15980777398 |
Product Overview
The Siemens 6SN1118-0DH22-0AA1 is a two-axis digital performance control unit for the SIMODRIVE 611-D drive system. It handles closed-loop control for digital drives used in feed-drive and main-spindle applications, with a direct measuring system that uses current signals. This configuration makes the exact model number important when matching a replacement to an existing CNC drive installation.
In a CNC machining center, the feed axes must follow programmed movements while the control system continuously evaluates feedback from the machine. The 6SN1118-0DH22-0AA1 supports this process by handling two controlled axes within the drive architecture. Depending on the machine configuration, the axes may control table movement, a tool slide, or another mechanism requiring coordinated motion.
A distinguishing feature of this model is its direct measuring system configuration. Where the machine uses a separate linear or direct position measuring device, the feedback arrangement can reflect movement at the measured machine axis rather than relying solely on motor-side feedback. This is particularly relevant when investigating positioning accuracy, following errors, and mechanical effects between the motor and the working axis.
The unit also supports digital drive control with a digital speed/torque setpoint interface. Its role is different from that of the drive power module: the control unit handles the control functions, while the associated power hardware supplies the energy required by the connected motor. Both parts must match the intended drive configuration.
For maintenance and replacement work, the 6SN1118-0DH22-0AA1 should be identified by its complete order number and feedback specification. Other SIMODRIVE 611-D control units may have a different number of axes, measuring-system arrangement, or signal type. Similar appearance or membership in the same product family is not sufficient to establish interchangeability.
Technical Specifications
| Parameter | Specification |
|---|---|
| Manufacturer | Siemens |
| Model | 6SN1118-0DH22-0AA1 |
| Product Family | SIMODRIVE 611 |
| Drive System | SIMODRIVE 611-D |
| Product Type | Closed-Loop Plug-In Performance Control Unit |
| Number of Axes | 2 |
| Drive Type | Digital drives |
| Control Application | Feed-drive and main-spindle drive control |
| Control Interface | Digital speed/torque setpoint interface |
| Measuring System | Direct measuring system |
| Measuring-System Signal Type | Current signals |
| Control Function | Digital closed-loop drive control |
| Installation Type | Plug-in control unit |
| Typical Application | CNC machine tools and industrial motion-control systems |
| Dimensions | 330 × 51 × 152 mm |
| Weight | 0.84 kg |
Product Features
- Two-axis digital control: Handles two controlled axes within a compatible SIMODRIVE 611-D drive configuration.
- Performance closed-loop control: Supports demanding feed-drive and main-spindle control applications.
- Direct measuring system interface: Accommodates the specified direct feedback arrangement.
- Current-signal feedback: Distinguishes this version from related control units configured for voltage-signal measuring systems.
- Digital speed/torque setpoint interface: Supports the associated digital drive-control architecture.
- Feed and spindle applications: Fits machine configurations that require controlled axis movement or spindle-drive operation.
- Plug-in drive integration: Works as part of the SIMODRIVE 611-D system rather than as a standalone drive.
- Variant-specific configuration: Requires matching the control unit to the existing drive hardware and feedback arrangement.
Working Principle
The 6SN1118-0DH22-0AA1 participates in the closed-loop control process between the CNC controller, drive power hardware, motor, and measuring system. The higher-level controller specifies the required movement, while the control unit processes the drive-control commands and feedback associated with the configured axes.
A simplified control path is:
CNC Controller → 6SN1118-0DH22-0AA1 → SIMODRIVE Power Module → Motor → Machine Axis
Direct Measuring System → Feedback Interface → Closed-Loop Control
When a CNC program commands a feed axis to move, the drive system converts the command into controlled motor movement. The direct measuring system reports the measured movement through the configured feedback interface. The control process uses this information to evaluate the difference between the commanded and measured response.
For example, during milling, a machine table may need to follow a programmed contour while cutting forces change throughout the operation. Feedback allows the control system to respond to deviations between the required and measured motion. The final positioning behavior depends on the complete drive configuration, mechanical transmission, measuring equipment, and control parameters.
The direct measuring system is an important consideration in this application. A measuring device installed along the machine axis can report movement at the measured location, helping the control system account for certain mechanical effects that may not be fully represented by motor-side feedback alone. The benefits depend on the actual machine mechanics and the correctly configured feedback loop.
The current-signal interface must also match the installed measuring equipment. A control unit configured for voltage signals should not be treated as interchangeable without verifying the feedback hardware and electrical specifications. During troubleshooting, technicians should therefore check the measuring-system type, signal wiring, axis assignment, and associated drive hardware before changing control parameters.
Role in a SIMODRIVE 611-D Drive Architecture
The 6SN1118-0DH22-0AA1 functions as the control element for two axes in a SIMODRIVE 611-D installation. It works with the power modules, motors, measuring systems, and CNC controller to coordinate machine movement.
CNC Controller → Digital Control Unit → Drive Power Module → Motor → Feed Axis or Spindle
Direct Measuring System → Feedback Interface → Control Unit
| System Element | Function |
|---|---|
| 6SN1118-0DH22-0AA1 | Performs closed-loop control for two axes using the specified direct measuring system configuration |
| SIMODRIVE 611 Power Module | Supplies electrical power to the associated drive motor |
| Feed-Drive Motor | Produces controlled mechanical movement for a machine axis |
| Main-Spindle Drive Components | Support spindle rotation where the system configuration assigns the relevant control functions |
| Direct Measuring System | Measures movement at the configured machine location |
| CNC Controller | Generates motion commands and coordinates machining operations |
| Machine-Axis Mechanics | Transmit motor movement to the table, slide, or other controlled element |
| Feedback Wiring | Carries measuring-system signals to the control interface |
Correct integration depends on the number of controlled axes, the installed power hardware, the feedback signal type, and the machine’s control configuration. These elements should be checked together during replacement or commissioning.
Industrial Applications
| Application | Typical Use |
|---|---|
| CNC Milling Machines | Regulating feed-axis movement during cutting and contour machining |
| CNC Turning Centers | Controlling configured axes during turning operations |
| Machining Centers | Coordinating two digital axes within a larger CNC system |
| Precision Machine Tools | Using direct measuring-system feedback for machine-axis control |
| Grinding Machines | Controlling feed movement where accurate positioning is required |
| Special-Purpose Machine Tools | Integrating digital closed-loop control into dedicated production equipment |
| CNC Retrofit Projects | Replacing a control unit after verifying the original feedback configuration |
| Automated Machining Cells | Coordinating machine movement with the higher-level control system |
| Feed-Drive Systems | Regulating the movement of tables, slides, and other machine axes |
| Drive Maintenance Applications | Investigating feedback errors, positioning deviations, and axis-control faults |
Installation and Maintenance
- Verify the complete order number: Confirm that the replacement is 6SN1118-0DH22-0AA1. Related SIMODRIVE control units can differ in axis count, feedback type, and supported drive functions.
- Check the drive-system configuration: Identify the installed SIMODRIVE 611-D power hardware, controlled axes, and CNC controller before removing the existing unit.
- Confirm the measuring-system type: Verify that the machine uses the direct measuring system arrangement associated with this model.
- Check current-signal compatibility: Confirm that the measuring device and feedback interface use the appropriate signal type before reconnecting the unit.
- Inspect feedback wiring: Check connectors, shielding, cable routing, and contact condition when positioning errors or feedback faults occur.
- Verify axis assignments: Ensure that the control unit’s two axes correspond to the intended machine movements and controller configuration.
- Review the established parameters: Check the machine’s commissioning records and existing drive configuration before changing control-loop or axis-related settings.
- Inspect the power module: If an axis fails to move correctly, check the associated drive power hardware and its status rather than assuming the control unit is responsible.
- Investigate following errors: Compare commanded movement with measured position and available drive diagnostics to help distinguish feedback faults from mechanical or drive-related problems.
- Examine mechanical transmission components: Check couplings, ball screws, linear guides, and other relevant mechanisms if the measured movement does not match the expected machine response.
- Follow electrical safety procedures: Isolate hazardous electrical energy and follow the machine’s approved servicing procedures before removing the plug-in control unit or handling drive connections.
- Record replacement details: Document the installed order number, feedback arrangement, axis assignments, parameter changes, and functional test results after servicing.
Compatible System Components
| Component | Function |
|---|---|
| Siemens SIMODRIVE 611-D Drive System | Provides the drive architecture for the control unit |
| Compatible SIMODRIVE 611 Power Module | Supplies power to the connected drive motor |
| Compatible Feed-Drive Motor | Converts electrical drive output into controlled axis movement |
| Compatible Main-Spindle Drive Components | Support spindle operation within the configured drive system |
| Direct Measuring System | Supplies feedback for the specified control configuration |
| CNC Controller | Generates motion commands and coordinates machining sequences |
| Feedback Signal Cables | Carry measuring-system signals to the control interface |
| Motor Power Cables | Connect the drive power hardware to the motor |
| Machine-Axis Mechanics | Transfer motor movement to the machine table, slide, or other controlled mechanism |
Recommended Related Models
| Model | Product Type | Configuration Consideration |
|---|---|---|
| Siemens 6SN1118-0DH22-0AA0 | SIMODRIVE 611-D Control Unit | Related two-axis configuration with direct measuring system and current signals; verify the precise control designation |
| Siemens 6SN1118-0DH21-0AA1 | SIMODRIVE 611-D Control Unit | Related two-axis variant; verify measuring-system configuration before selection |
| Siemens 6SN1118-0DH23-0AA1 | SIMODRIVE 611-D Closed-Loop Plug-In Performance Control Unit | Related direct measuring system variant using voltage signals |
| Siemens 6SN1118-0DG22-0AA1 | SIMODRIVE 611-D Control Unit | Related one-axis configuration with direct measuring system and current signals |
| Siemens SIMODRIVE 611-D | Digital Drive System | Drive platform for compatible digital feed and spindle-drive applications |
Key Advantages
- Controls two axes within a compatible SIMODRIVE 611-D drive system.
- Supports performance-oriented digital closed-loop control.
- Accommodates a direct measuring system using current signals.
- Supports feed-drive and main-spindle drive applications within the appropriate configuration.
- Integrates with compatible SIMODRIVE power hardware and CNC control systems.
Technical FAQs
What distinguishes the 6SN1118-0DH22-0AA1 from a control unit using voltage-signal feedback?
The 6SN1118-0DH22-0AA1 is associated with a direct measuring system using current signals. Related variants may use voltage signals instead. The feedback interface must match the measuring equipment installed on the machine, so the complete order number should be checked before replacement.
Can this control unit handle two feed axes in a CNC machine?
It is a two-axis control unit for the SIMODRIVE 611-D system. Its use for particular feed axes depends on the installed power modules, motor configuration, CNC controller, and machine setup.
Why might a machine report positioning errors after the control unit has been replaced?
Possible causes include an incompatible measuring-system signal type, incorrect feedback wiring, incorrect axis assignment, parameter mismatches, or mechanical problems. Confirming the control-unit variant and feedback arrangement is a sensible first step before making adjustments to the control loop.
What should be checked before installing this unit in an existing SIMODRIVE 611-D system?
Verify the complete order number, number of controlled axes, direct measuring system configuration, current-signal feedback, associated power modules, and machine parameter requirements. Matching the product family alone does not establish full system compatibility.